Stainless Steel Welding Guide: Process, Distortion, and Finish
Stainless Steel Welding Guide: Process, Distortion, and Finish is a practical engineering reference for teams that need manufacturable metal parts without hiding risk behind generic rules. The guide emphasizes grade identification, clean handling, process selection, heat input, shielding, joint access, and post-weld corrosion performance. The guide explains how to translate function into process choices, tolerances, inspection points, and supplier questions. It also shows where prototype evidence should replace assumptions. XCWY has supported metal-part production since 1998 and can combine stamping, deep drawing, laser cutting, bending, five-axis machining, welding, PEM insertion, finishing coordination, and CMM inspection. Available equipment includes 25–400-ton presses, a 12 kW laser, a 3,200 mm press brake, and a DMU38 five-axis center. The operating quality system is ISO 9001:2015, certificate 34025Q30296R0S. Use this stainless steel welding guide resource to prepare a clearer RFQ, compare feasible routes, and agree acceptance criteria before material or tooling is committed.
Request a Drawing Review
Attach the drawing, revision, material, quantity, critical tolerances, finish and target date. The inquiry is saved in the site database and emailed to the XCWY team.
Identify Grade and Service
Within stainless steel welding guide: process, distortion, and finish, treat identify grade and service as a controlled engineering choice rather than a drawing afterthought. Confirm stainless grade, product form, thickness, finish, corrosion environment, temperature, load, and applicable code before choosing consumables. Austenitic grades are common but still vary in chemistry and behavior; ferritic, martensitic, duplex, and precipitation-hardening grades require different controls. Prevent material mix-up through traceability and dedicated storage. A visually clean weld is not automatically suitable for every corrosive or structural service. When documenting identify grade and service, separate mandatory functional requirements from preferences, then identify the datums, interfaces, cosmetic zones, load paths, and acceptance evidence relevant to this decision. The drawing, CAD model, material callout, finish note, and revision should give one consistent definition of the identify grade and service requirement. Apply tight limits only where identify grade and service affects fit, motion, safety, sealing, or interchangeability; a blanket tolerance can add setup and inspection cost without improving performance. If uncertainty remains around identify grade and service, approve a representative first article before committing production material or tooling.
Select TIG, MIG, Laser, or Spot Welding
For stainless steel welding guide: process, distortion, and finish, resolve select tig, mig, laser, or spot welding before production data is released. TIG provides precise heat and clean appearance on thin sections but can be slower. MIG improves deposition and productivity on longer seams. Laser welding offers concentrated heat input and narrow seams when fit-up is controlled. Resistance spot welding suits overlapped sheet with accessible electrodes. XCWY offers these processes, but joint access, thickness, gap, load, appearance, volume, and qualification needs determine the route. When documenting select tig, mig, laser, or spot welding, separate mandatory functional requirements from preferences, then identify the datums, interfaces, cosmetic zones, load paths, and acceptance evidence relevant to this decision. The drawing, CAD model, material callout, finish note, and revision should give one consistent definition of the select tig, mig, laser, or spot welding requirement. Apply tight limits only where select tig, mig, laser, or spot welding affects fit, motion, safety, sealing, or interchangeability; a blanket tolerance can add setup and inspection cost without improving performance. If uncertainty remains around select tig, mig, laser, or spot welding, approve a representative first article before committing production material or tooling.
Control Heat and Distortion
In stainless steel welding guide: process, distortion, and finish, a review of control heat and distortion must connect geometry, material behavior, tooling access, and inspection. Stainless has relatively low thermal conductivity and high thermal expansion, making heat concentration and distortion important. Use balanced sequences, intermittent welds where sealing is unnecessary, suitable fixtures, controlled travel, and the minimum heat input consistent with fusion. Leave room for shrinkage in tolerance analysis. Pre-setting may help repeat work, but it should be based on measured behavior rather than arbitrary reverse deformation. When documenting control heat and distortion, separate mandatory functional requirements from preferences, then identify the datums, interfaces, cosmetic zones, load paths, and acceptance evidence relevant to this decision. The drawing, CAD model, material callout, finish note, and revision should give one consistent definition of the control heat and distortion requirement. Apply tight limits only where control heat and distortion affects fit, motion, safety, sealing, or interchangeability; a blanket tolerance can add setup and inspection cost without improving performance. If uncertainty remains around control heat and distortion, approve a representative first article before committing production material or tooling.
Prevent Contamination and Corrosion Loss
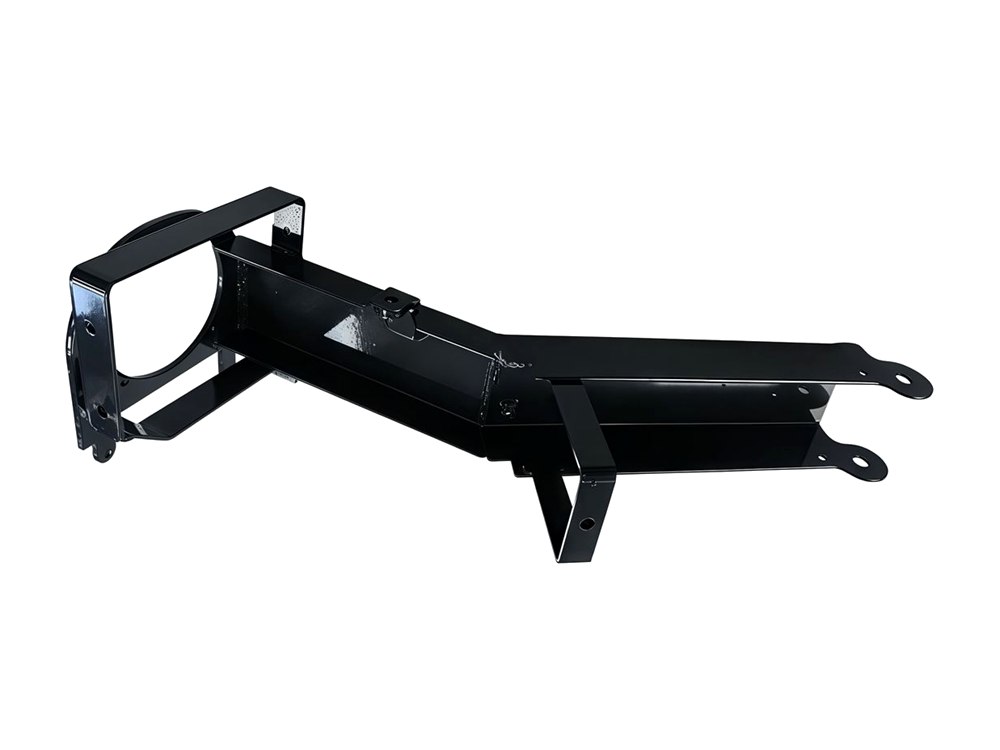
Within stainless steel welding guide: process, distortion, and finish, treat prevent contamination and corrosion loss as a controlled engineering choice rather than a drawing afterthought. Keep carbon-steel grinding dust, wire brushes, clamps, and benches away from stainless surfaces. Use dedicated tools and clean gloves, then remove oils and marking residues near the joint. Shield the weld pool correctly; purge the root when oxidation there would impair corrosion or cleanliness. Excessive heat tint signals oxidation and may require removal and passivation according to the service specification. When documenting prevent contamination and corrosion loss, separate mandatory functional requirements from preferences, then identify the datums, interfaces, cosmetic zones, load paths, and acceptance evidence relevant to this decision. The drawing, CAD model, material callout, finish note, and revision should give one consistent definition of the prevent contamination and corrosion loss requirement. Apply tight limits only where prevent contamination and corrosion loss affects fit, motion, safety, sealing, or interchangeability; a blanket tolerance can add setup and inspection cost without improving performance. If uncertainty remains around prevent contamination and corrosion loss, approve a representative first article before committing production material or tooling.
Design the Joint and Fit-Up
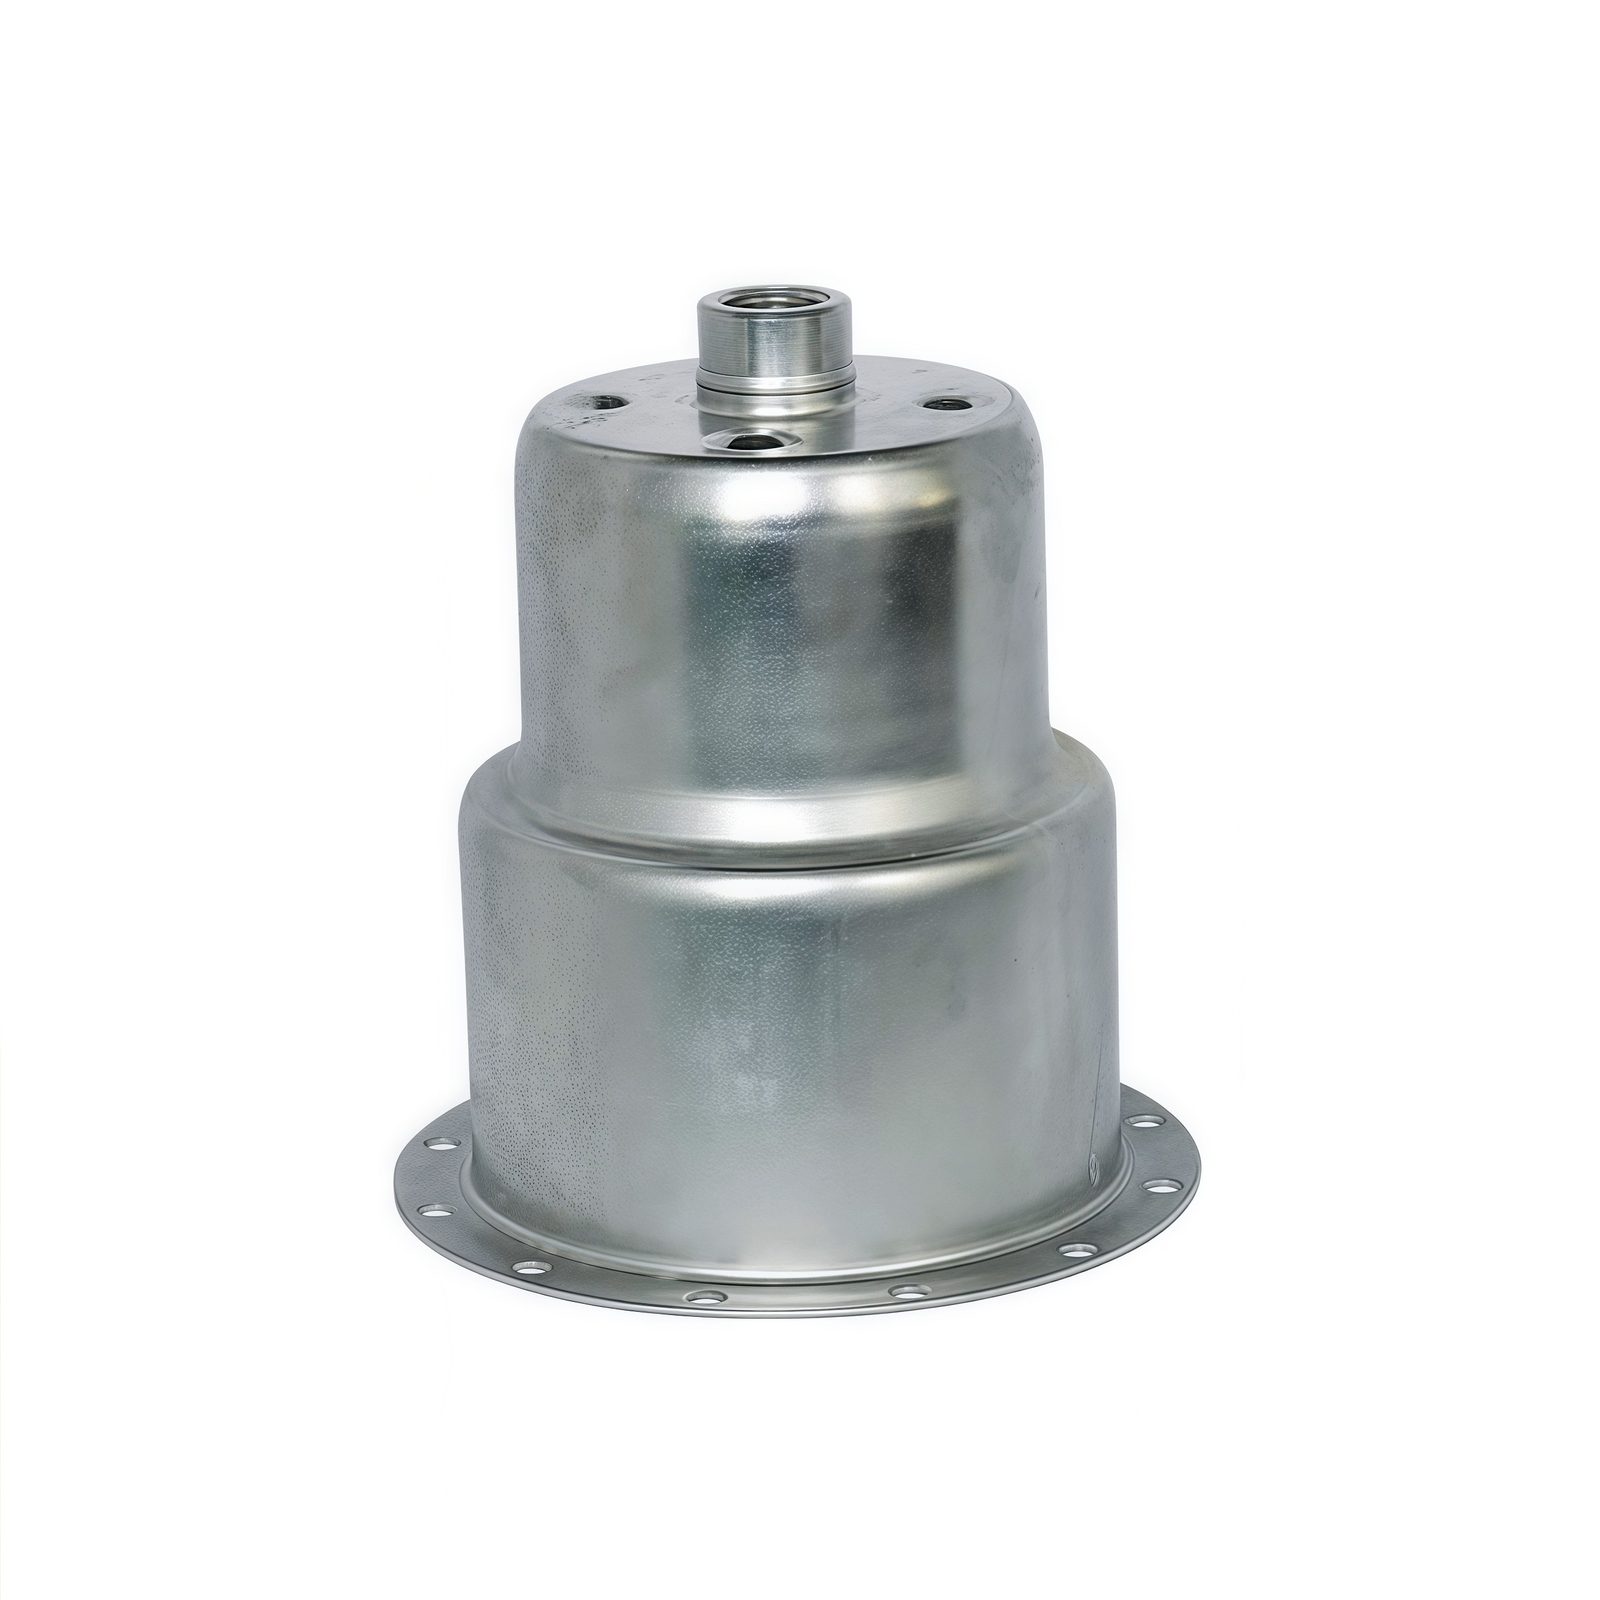
For stainless steel welding guide: process, distortion, and finish, resolve design the joint and fit-up before production data is released. Select butt, lap, corner, or fillet geometry from load path, access, sealing, and finish. Consistent root opening and edge preparation are essential, especially for laser welding and automated travel. Avoid inaccessible crevices in wet or hygienic service. Size welds to calculation or governing standard rather than over-welding, which adds heat and finishing. Call out start-stop treatment and acceptable undercut, porosity, and mismatch. When documenting design the joint and fit-up, separate mandatory functional requirements from preferences, then identify the datums, interfaces, cosmetic zones, load paths, and acceptance evidence relevant to this decision. The drawing, CAD model, material callout, finish note, and revision should give one consistent definition of the design the joint and fit-up requirement. Apply tight limits only where design the joint and fit-up affects fit, motion, safety, sealing, or interchangeability; a blanket tolerance can add setup and inspection cost without improving performance. If uncertainty remains around design the joint and fit-up, approve a representative first article before committing production material or tooling.
Inspect and Finish Welds
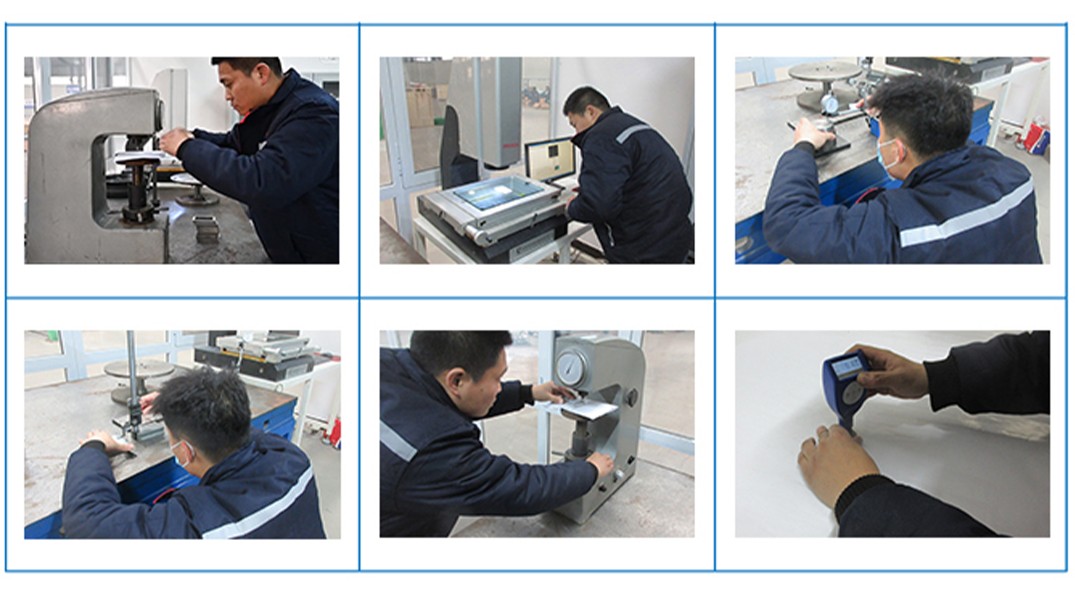
In stainless steel welding guide: process, distortion, and finish, a review of inspect and finish welds must connect geometry, material behavior, tooling access, and inspection. Inspection may combine visual examination, dimensional checks, dye penetrant, leak testing, or other methods required by service. Define acceptance standards and personnel qualifications when regulated work applies. Grinding can improve appearance but may thin the joint or smear contamination; establish a maximum profile and grain direction. Verify distortion after cooling and after finishing, then protect the restored surface during packing and assembly. When documenting inspect and finish welds, separate mandatory functional requirements from preferences, then identify the datums, interfaces, cosmetic zones, load paths, and acceptance evidence relevant to this decision. The drawing, CAD model, material callout, finish note, and revision should give one consistent definition of the inspect and finish welds requirement. Apply tight limits only where inspect and finish welds affects fit, motion, safety, sealing, or interchangeability; a blanket tolerance can add setup and inspection cost without improving performance. If uncertainty remains around inspect and finish welds, approve a representative first article before committing production material or tooling.
Engineering Decision Table
| Condition | Recommendation | Why |
|---|---|---|
| Unproven geometry—stainless steel welding guide | Run a representative prototype | Evidence reveals springback, distortion, access, and inspection risks in stainless steel welding guide. |
| Functional characteristic—stainless steel welding guide | Define datum-based measurement | Critical stainless steel welding guide controls need unambiguous acceptance evidence. |
| Cosmetic-only feature—stainless steel welding guide | Set an appearance-zone limit | A bounded stainless steel welding guide standard avoids unnecessary precision cost. |
| Low volume or changing design—stainless steel welding guide | Defer dedicated tooling | A flexible stainless steel welding guide route preserves revision freedom. |
| Stable repeat demand—stainless steel welding guide | Evaluate dedicated tooling or gauges | Upfront stainless steel welding guide engineering can reduce cycle time and variation. |
| Approved input changes—stainless steel welding guide | Perform a documented delta review | Substitution can change stainless steel welding guide dimensions, corrosion, or appearance. |
| Sector certification required—stainless steel welding guide | Confirm compliance before sourcing | XCWY does not claim ISO 13485, IATF 16949, AS9100, or UL. |
RFQ and Drawing Checklist
- Define the functional objective and failure modes—stainless steel welding guide.
- Attach matching 3D and revision-controlled 2D files—stainless steel welding guide.
- State material grade, temper, thickness, and substitution rules—stainless steel welding guide.
- Identify datums and critical-to-function dimensions—stainless steel welding guide.
- Separate cosmetic surfaces from nonappearance zones—stainless steel welding guide.
- Specify edge break, burr direction, and sharp-edge restrictions—stainless steel welding guide.
- Call out finish standard, color, gloss, masking, and test method—stainless steel welding guide.
- Provide prototype, launch, and expected annual quantities—stainless steel welding guide.
- Agree measurement equipment, sampling, and report format—stainless steel welding guide.
- Confirm joining hardware, weld symbols, and assembly sequence—stainless steel welding guide.
- Review packaging protection for surfaces and formed features—stainless steel welding guide.
- Resolve open DFM questions before approving material or tooling—stainless steel welding guide.
Manufacturing Evidence — Stainless Steel Welding
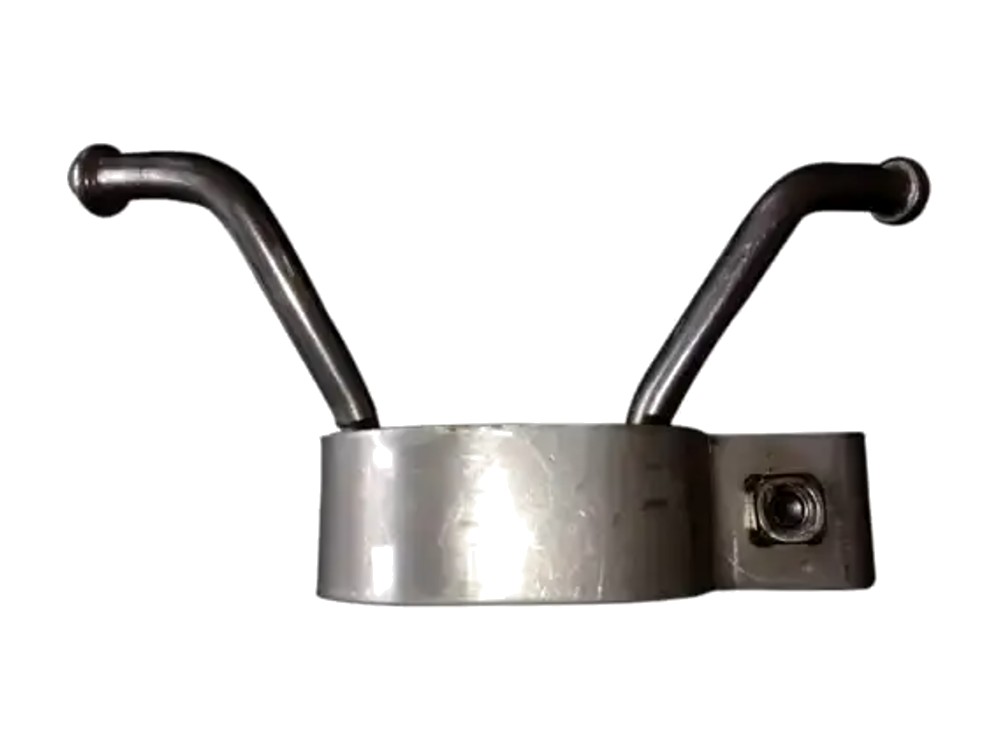
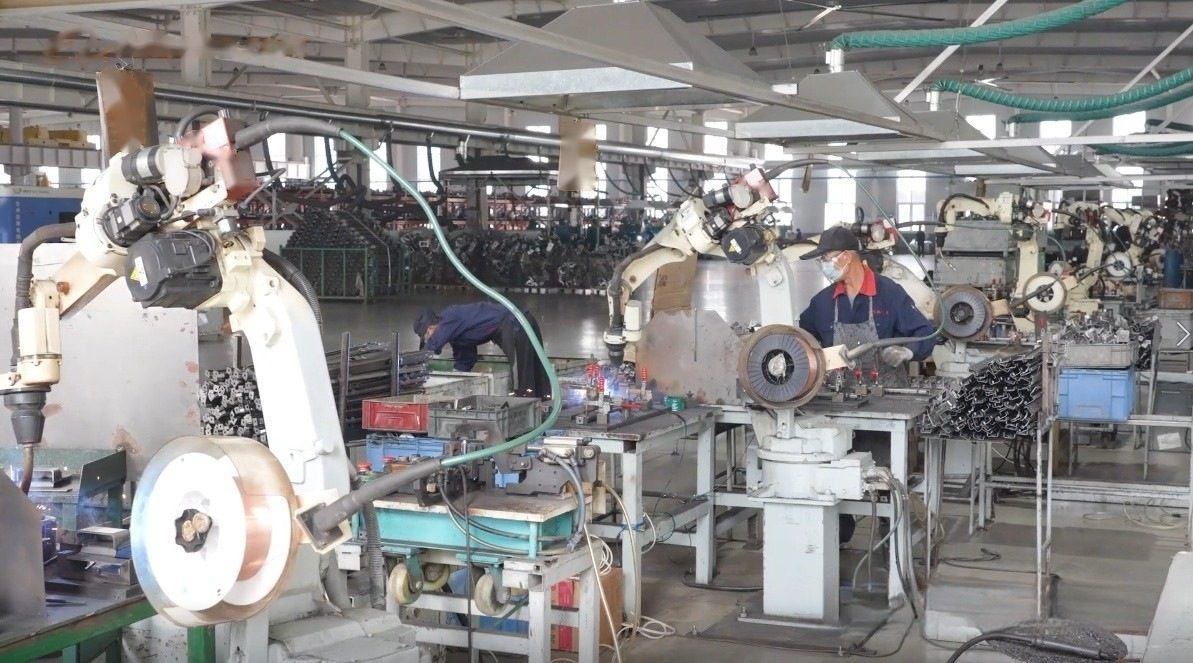
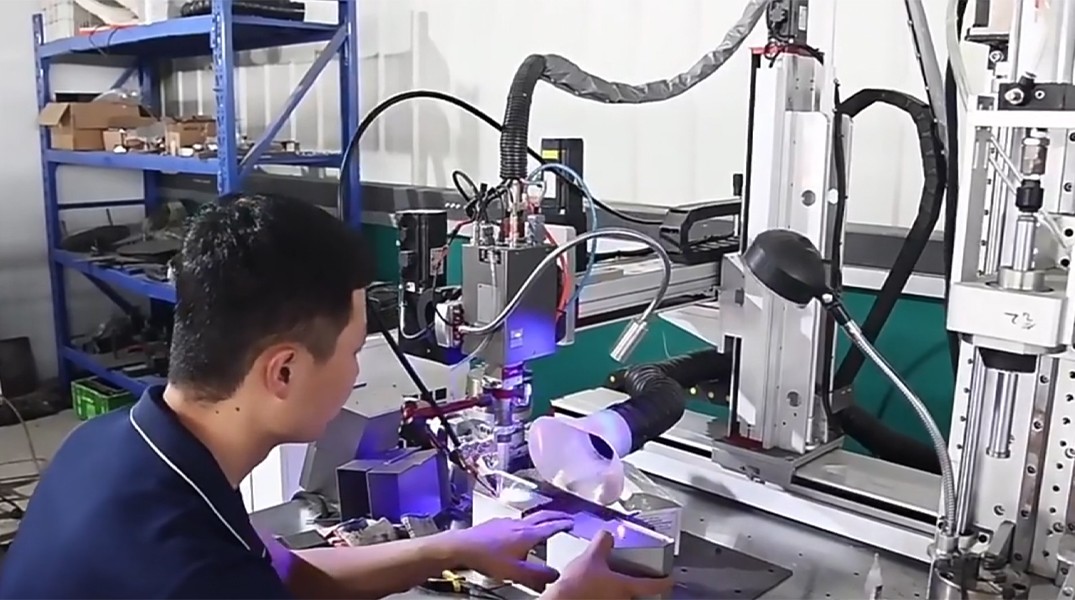
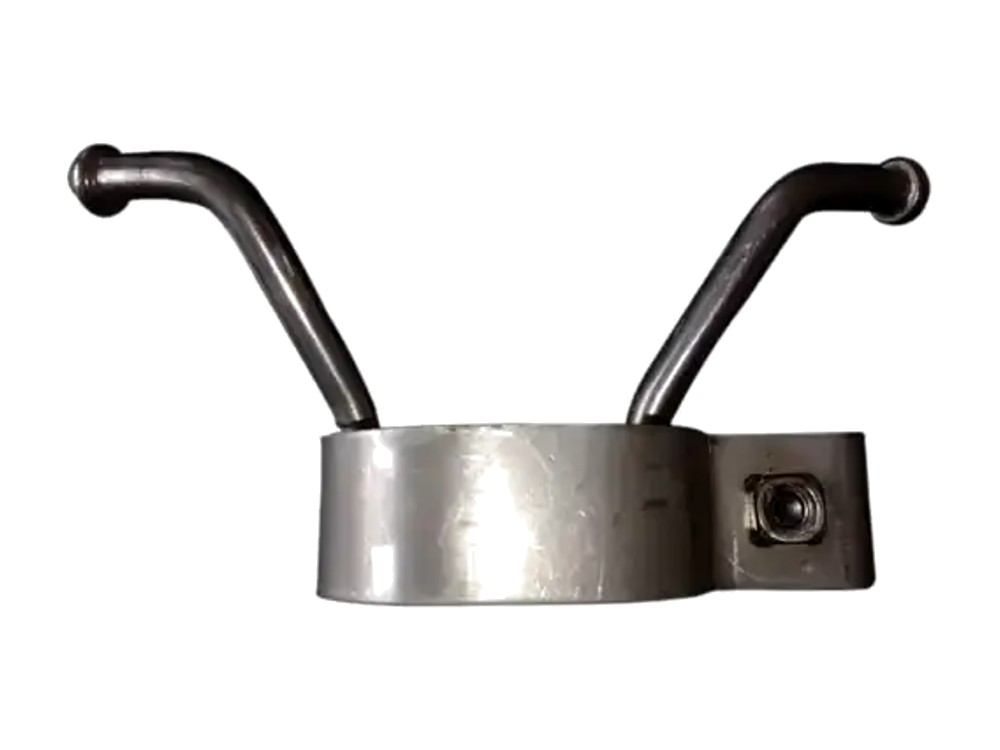
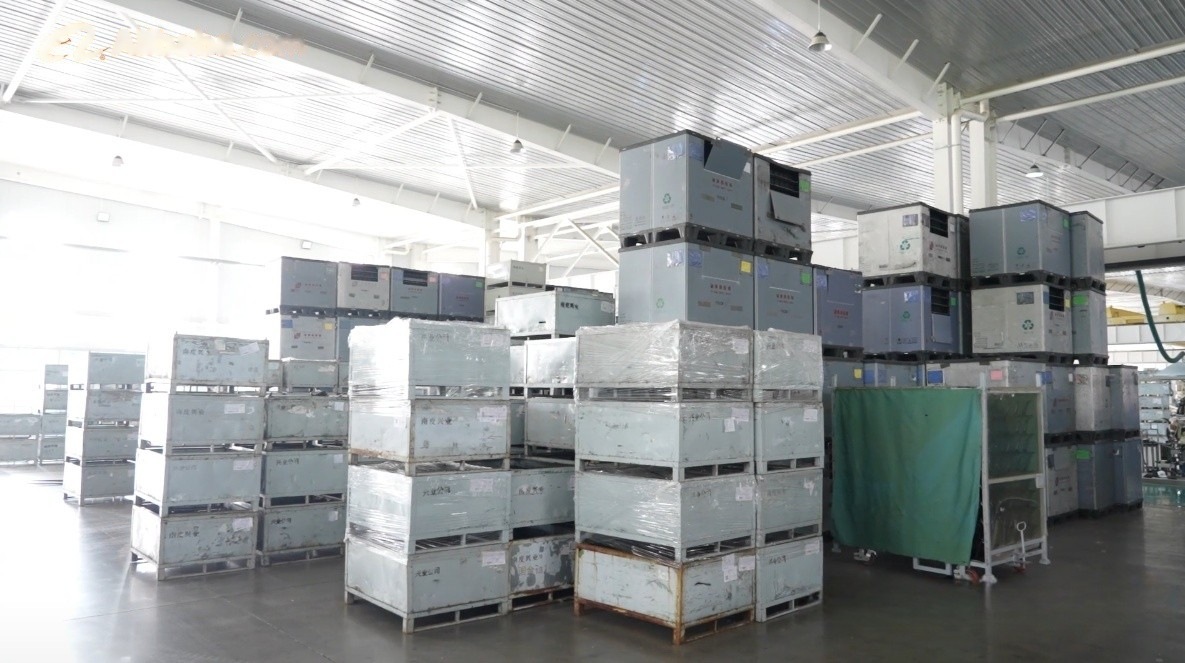
The images below come from the XCWY site asset library and show the plant, equipment, inspection areas and representative parts already published for Stainless Steel Welding.
Frequently Asked Questions
When should an engineer request DFM feedback for stainless steel welding guide?
Request stainless steel welding guide feedback before freezing the drawing and after any material, tolerance, finish, or volume change. An early stainless steel welding guide review leaves room to alter geometry before tooling or purchase orders are released.
What files make a stainless steel welding guide RFQ technically complete?
For stainless steel welding guide, provide matching 3D and controlled 2D data, material grade and temper, quantities, finish, critical dimensions, inspection expectations, and assembly context.
Can XCWY support one stainless steel welding guide prototype?
XCWY offers MOQ 1 when the selected stainless steel welding guide route is practical. A flexible prototype route may be proposed before production tooling is justified for stainless steel welding guide.
How quickly can XCWY quote a stainless steel welding guide project?
XCWY targets a stainless steel welding guide quotation within three business hours after receiving a complete package. Unclear stainless steel welding guide specifications, missing models, or complex tooling require clarification first.
Which quality certification applies to stainless steel welding guide?
Work involving stainless steel welding guide operates under XCWY’s ISO 9001:2015 system, certificate 34025Q30296R0S. For stainless steel welding guide, XCWY does not claim ISO 13485, IATF 16949, AS9100, or UL certification.
What is the most important project-specific check for stainless steel welding guide?
Confirm alloy, filler, heat input, shielding or purge, cleanliness, and post-weld treatment against the actual corrosion service; appearance alone cannot establish weld integrity.
Related XCWY Capabilities
Get a Manufacturing Review and Quote
Attach the drawing, revision, material, quantity, critical tolerances, finish and target date. The inquiry is saved in the site database and emailed to the XCWY team.