Custom Metal Assembly and Sub-Assembly Services
XCWY supports sourcing joined, fitted, and partially completed metal units through custom metal assembly built around drawings, stated requirements, and an agreed manufacturing route. For custom metal assembly, Nanpi Xinchengweiye Hardware Products Co., Ltd. For assemblies, brings operations dating from 1998, a 15,000 m² facility, six lines, and 78 employees. The central capability is combining formed or machined components through laser, TIG, MIG, or spot welding, PEM insertion, and controlled sub-assembly. Relevant resources span 25–400 ton presses, 12,000 W fiber laser cutting, the 3,200 mm JFY TPR8-100 CNC press brake rated to ±0.5°, the HDL-OKK DMU38 five-axis platform rated to ±0.005 mm, four welding methods, PEM insertion, sub-assembly, and CMM inspection for custom metal assembly. For assemblies, mOQ starts at one piece, with an NDA on request and quotation response within three business hours. For assemblies, send drawings, material, quantity, finish, and inspection priorities to review the route.
Request a Drawing Review
Attach the drawing, revision, material, quantity, critical tolerances, finish and target date. The inquiry is saved in the site database and emailed to the XCWY team.
Define the custom metal assembly requirement
A useful custom metal assembly inquiry begins with function, not only geometry. For assemblies, xCWY reviews the drawing together with material designation, expected quantity, surface requirement, critical features, and the relationship between mating parts. The purpose is to choose a route that reflects sourcing joined, fitted, and partially completed metal units. For custom metal assembly, that route may combine combining formed or machined components through laser, TIG, MIG, or spot welding, PEM insertion, and controlled sub-assembly. For assemblies, processes are selected according to the released definition; the availability of a machine does not by itself mean every tolerance, thickness, or shape is appropriate for that process. For assemblies, buyers should identify dimensions that govern fit, sealing, alignment, movement, or downstream assembly, while separating them from noncritical dimensions. The supported material list for custom metal assembly includes cold rolled steel, galvanized steel, SS304, SS316, SS316L, AL5052, AL6061-T6, C110 copper, and C260 brass. For assemblies, grade and temper should be written directly on the drawing or purchase specification, because family names alone can conceal meaningful differences in forming, machining, welding, conductivity, corrosion behavior, and finish response. For assemblies, xCWY can start from an MOQ of one piece, which allows the commercial path to match prototypes, short runs, or repeat programs. For assemblies, a three-business-hour quotation response helps establish the first commercial view, but manufacturability still depends on usable files and clear requirements. For assemblies, an NDA can be requested before sensitive project information is exchanged.
Select processes around the part
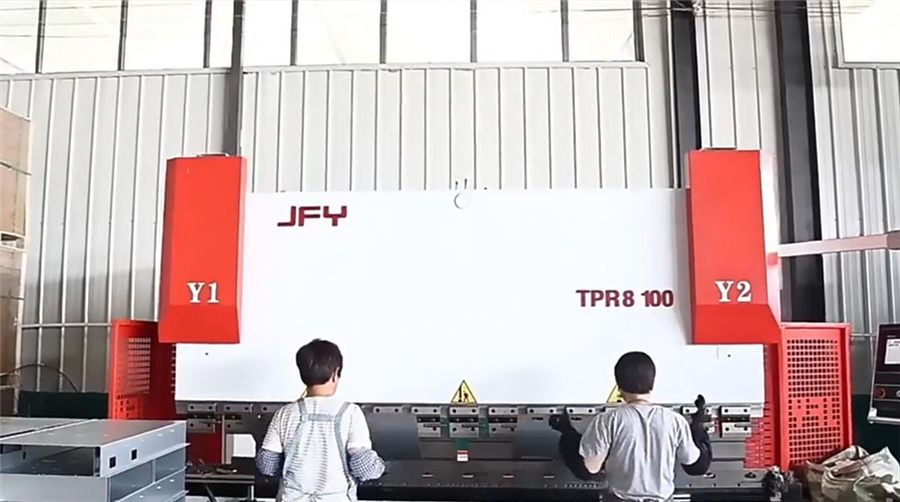
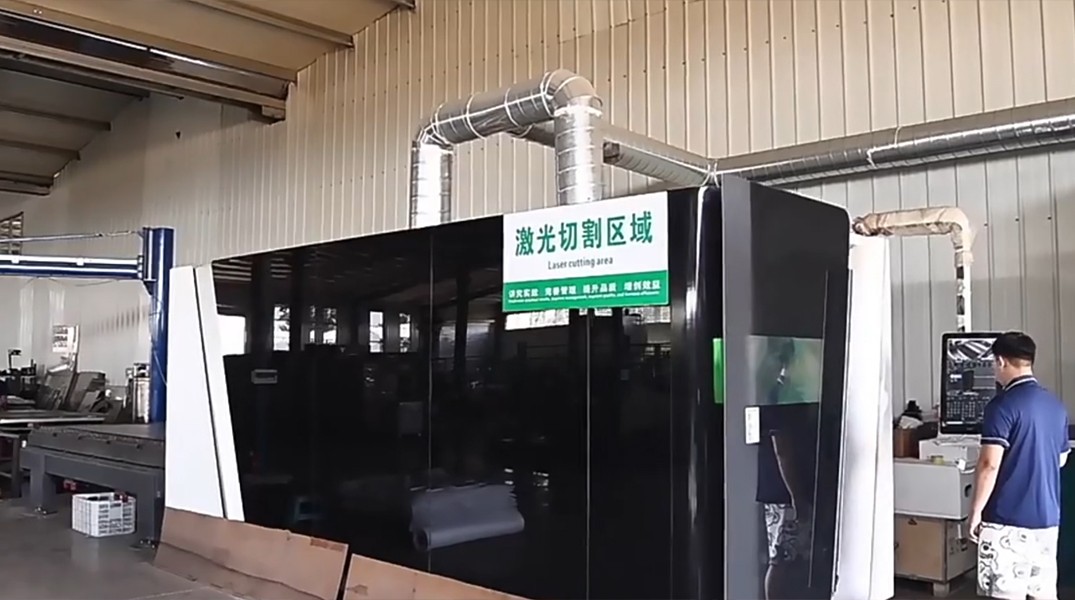
Process selection for custom metal assembly should follow the part rather than a fixed menu. For assemblies, xCWY has presses rated from 25 to 400 tons for stamping and forming work, plus a 12,000 W fiber laser for profile cutting. For assemblies, published laser capacities are carbon steel to 25 mm, stainless steel to 20 mm, aluminum to 12 mm, and copper to 6 mm. For assemblies, these figures describe equipment capability, not an automatic promise that every contour and tolerance is feasible at the maximum thickness. Bending for custom metal assembly can be reviewed around the JFY TPR8-100 CNC press brake, with a 3,200 mm working length and a stated angular capability of ±0.5°. For assemblies, feature position, flange length, bend relief, grain direction, and springback assumptions should be assessed together. For assemblies, where milled faces, pockets, holes, or multi-side access are needed, the HDL-OKK DMU38 five-axis machine carries a stated capability of ±0.005 mm. For assemblies, the applicable part tolerance must still be agreed from geometry, datum structure, material, and inspection method. Joining options for custom metal assembly include laser, TIG, MIG, and spot welding. For assemblies, pEM insertion and sub-assembly can be added when the drawing defines hardware type, orientation, access, and acceptance conditions. This process range gives a procurement or engineering team that wants assembly responsibility defined before tooling or fabrication begins a practical basis for comparing one-process and combined-process solutions.
Control material and surface expectations
Material and finish notes strongly influence custom metal assembly. For assemblies, xCWY lists cold rolled steel, Q235, galvanized steel, SS304, SS316, SS316L, AL5052, AL6061-T6, C110 copper, C260 brass, and 65Mn among its available materials. For assemblies, the quotation should reference a specific grade, thickness or stock form, and any required condition instead of allowing an undefined equivalent. For assemblies, that discipline is especially important when a design relies on bend response, hardness, corrosion behavior, conductivity, weldability, or cosmetic appearance. Listed finish routes for custom metal assembly include powder coating, zinc plating, anodizing, brushing, polishing, and passivation. For assemblies, not every finish applies to every metal, so the requested combination must be reviewed. For assemblies, drawings should state color or appearance criteria where relevant, masked or contact areas, visible faces, grain direction for brushed surfaces, and whether dimensional requirements apply before or after finishing. For assemblies, threads, PEM hardware, tight fits, and electrical contact zones may need explicit protection instructions. For assemblies, finish language such as “standard,” “clean,” or “good appearance” is too open for dependable sourcing. A better custom metal assembly package separates functional protection from cosmetic expectations and identifies inspection lighting or reference samples only when the buyer actually supplies or approves them. For assemblies, xCWY can then align fabrication sequence, handling, and outsourced or in-house finish coordination with the stated requirement without inventing an acceptance level.
Plan inspection and qualification
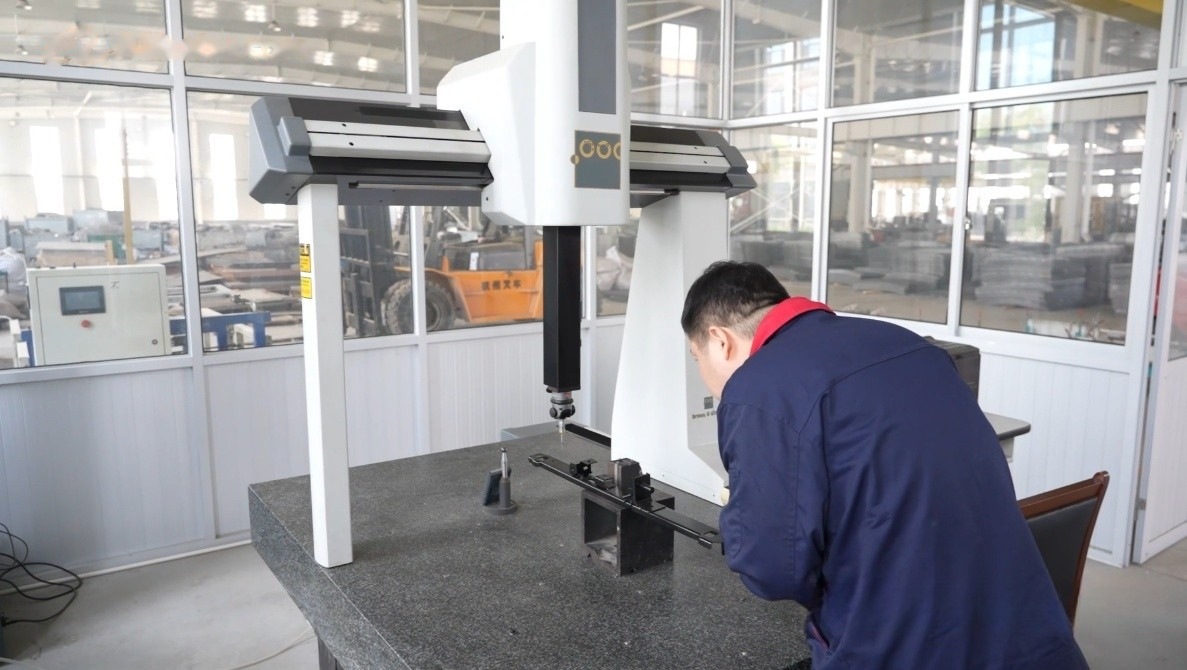
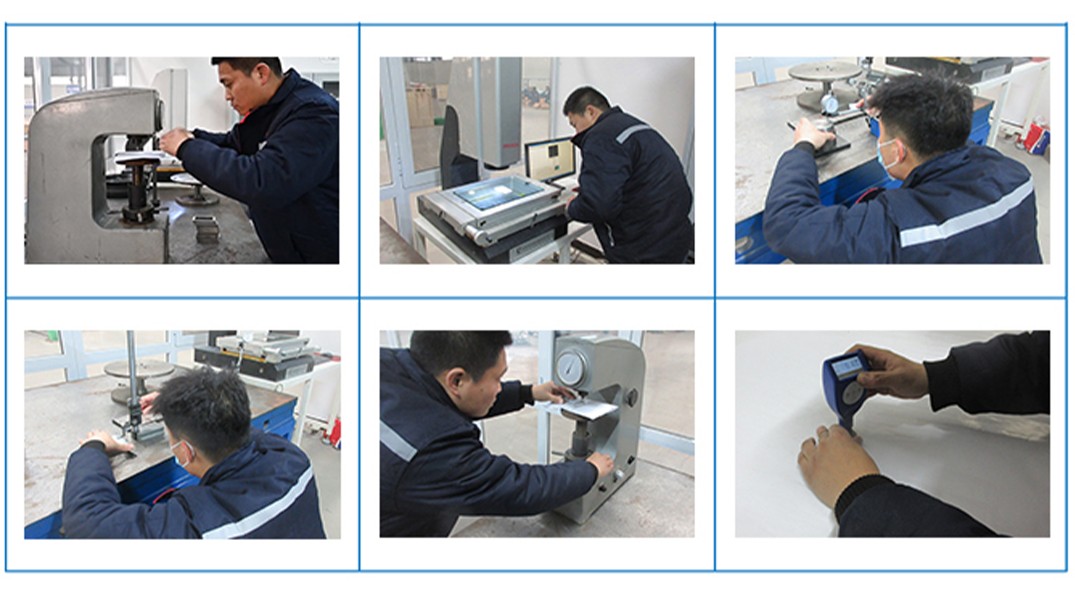
Quality planning for custom metal assembly starts before the first cut. For assemblies, xCWY operates under ISO 9001:2015 registration 34025Q30296R0S and has CMM inspection capability. For assemblies, the registration supports a quality-management framework, while the drawing and purchase requirements still define what must be measured for the specific order. For assemblies, buyers should mark critical-to-function characteristics, datum references, thread requirements, weld expectations, finish checkpoints, and any records requested with the shipment. A CMM can support dimensional verification for suitable custom metal assembly features, but inspection method must fit accessibility, surface condition, tolerance, and part stability. For assemblies, not every characteristic is best measured on a CMM, and the presence of inspection equipment should not be interpreted as an unstated guarantee for all dimensions. For assemblies, a clear inspection plan identifies sampling or full-check expectations, measurement stage, and the document format needed for review. For assemblies, xCWY does not claim ISO 13485, IATF 16949, AS9100, or UL certification. For assemblies, projects that contractually require one of those credentials should not treat ISO 9001:2015 as a substitute. For a procurement or engineering team that wants assembly responsibility defined before tooling or fabrication begins, this transparent boundary makes qualification more efficient: confirm whether the stated ISO registration and available process controls satisfy the program, then place any additional verification obligations directly in the inquiry and purchase documents.
Build a quotation-ready RFQ
To request a useful custom metal assembly quotation, provide 2D drawings and available 3D data, revision level, material and thickness, order quantity, annual or repeat expectations if known, finish, hardware, weld notes, and inspection priorities. For assemblies, identify whether the request is for a one-piece evaluation, a low-volume batch, or recurring production. For assemblies, xCWY offers quotation response within three business hours when the information is sufficient, and the MOQ starts from one piece. For assemblies, an NDA is available on request for confidential files. For assemblies, the first review should resolve interfaces that drive risk: datums, mating locations, bend orientation, weld access, tool access, edge condition, hardware direction, visible surfaces, and packaging-sensitive areas. For custom metal assembly, changes should be recorded by revision rather than mixed through informal messages. For assemblies, if an alternative process is proposed, the buyer should approve any effect on geometry, material condition, finish, or inspection before release. This structured RFQ approach serves sourcing joined, fitted, and partially completed metal units because commercial and technical assumptions become visible at the same time. For assemblies, it also gives XCWY a basis for deciding whether stamping, laser cutting, bending, five-axis machining, welding, insertion, sub-assembly, or a combination is appropriate. For assemblies, the result is not a generic capability claim; it is a traceable proposal tied to the submitted part definition and requested quantity.
Specifications and Scope
| Company history | Operating since 1998 |
|---|---|
| Quality system | ISO 9001:2015, registration 34025Q30296R0S |
| Facility | 15,000 m² |
| Production resources | 6 lines and 78 employees |
| Press range | 25–400 ton |
| Fiber laser | 12,000 W; carbon steel 25 mm, stainless 20 mm, aluminum 12 mm, copper 6 mm |
| CNC press brake | JFY TPR8-100, 3,200 mm, ±0.5° |
| Five-axis CNC | HDL-OKK DMU38, ±0.005 mm |
| Joining | Laser, TIG, MIG, and spot welding |
| Secondary operations | PEM insertion and sub-assembly |
| Inspection | CMM capability |
| Commercial access | MOQ from 1 piece; quotation within 3 business hours; NDA on request |
Typical Applications
Welded equipment frames
Use custom metal assembly to source drawing-defined welded equipment frames when material, critical interfaces, finish, quantity, and inspection priorities are stated in the RFQ.
Fastener-equipped panels
For fastener-equipped panels, XCWY can review whether cutting, forming, machining, joining, insertion, or sub-assembly best matches the released geometry and order volume.
Bracket sub-assemblies
Buyers of bracket sub-assemblies can start at one piece, then request a separate route for repeat quantities if tooling or process economics should change.
Cabinet and box structures
A cabinet and box structures inquiry should identify mating points, visible surfaces, hardware, weld conditions, and the measurements that determine functional acceptance.
Mixed-process housings
XCWY evaluates mixed-process housings against its listed materials, equipment limits, finishes, and CMM capability rather than applying an assumed universal tolerance.
Production-ready modules
Procurement teams can place production-ready modules within a controlled custom metal assembly package by fixing revision, quantity, finish, and inspection scope before release.
Risks Buyers Should Resolve Before Release
| Risk | Effect | Control |
|---|---|---|
| Weld distortion | The custom metal assembly order may be built to conflicting requirements, causing avoidable clarification or rework. | Freeze the drawing revision and identify one owner for approved technical changes before manufacturing release for this custom metal assembly program. |
| Incorrect hardware placement | Functional interfaces may not align even when individual custom metal assembly features appear acceptable in isolation. | Mark critical characteristics and agree the relevant process, datum basis, and inspection method during quotation review for this custom metal assembly program. |
| Stack-up misalignment | The delivered surface or material behavior may differ from the buyer’s unstated expectation for custom metal assembly. | Specify material grade, stock condition, finish, visible faces, and protected areas directly in controlled documents for this custom metal assembly program. |
| Mixed revision components | Process interaction may shift geometry or complicate access on the custom metal assembly part or assembly. | Review forming, machining, and joining sequence against access, heat input, springback, and accumulated variation for this custom metal assembly program. |
| Cosmetic damage during joining | Parts may be difficult to accept consistently or may be damaged after otherwise conforming custom metal assembly work. | Define packaging-sensitive surfaces and confirm the required inspection records, sampling approach, and acceptance language for this custom metal assembly program. |
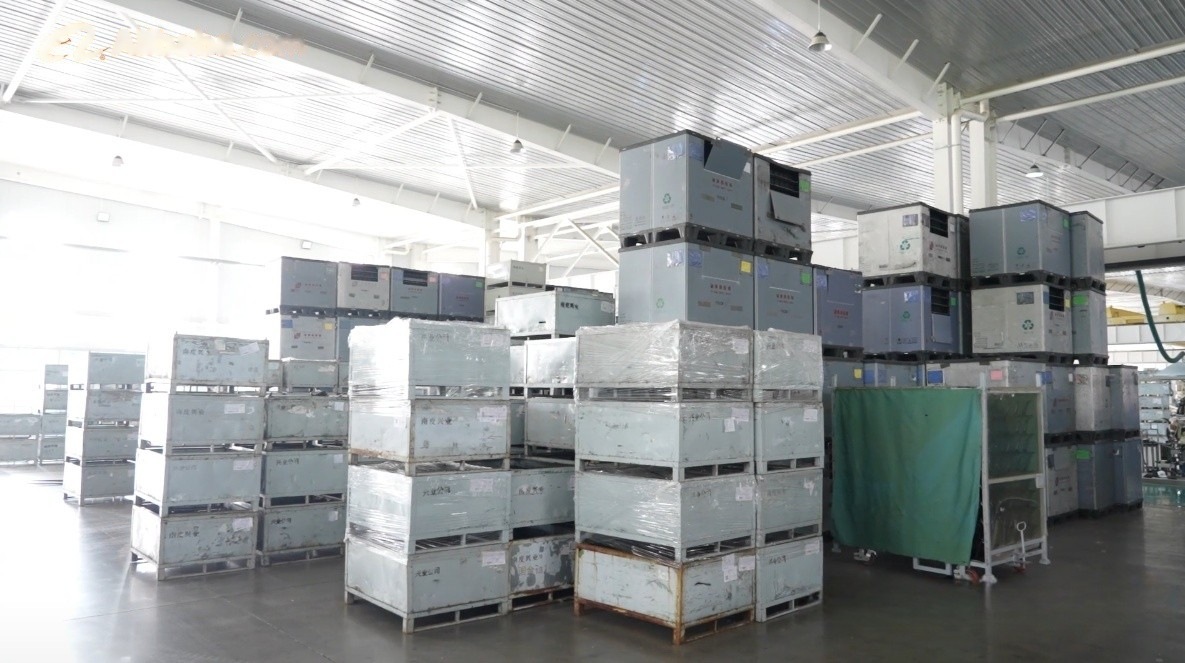
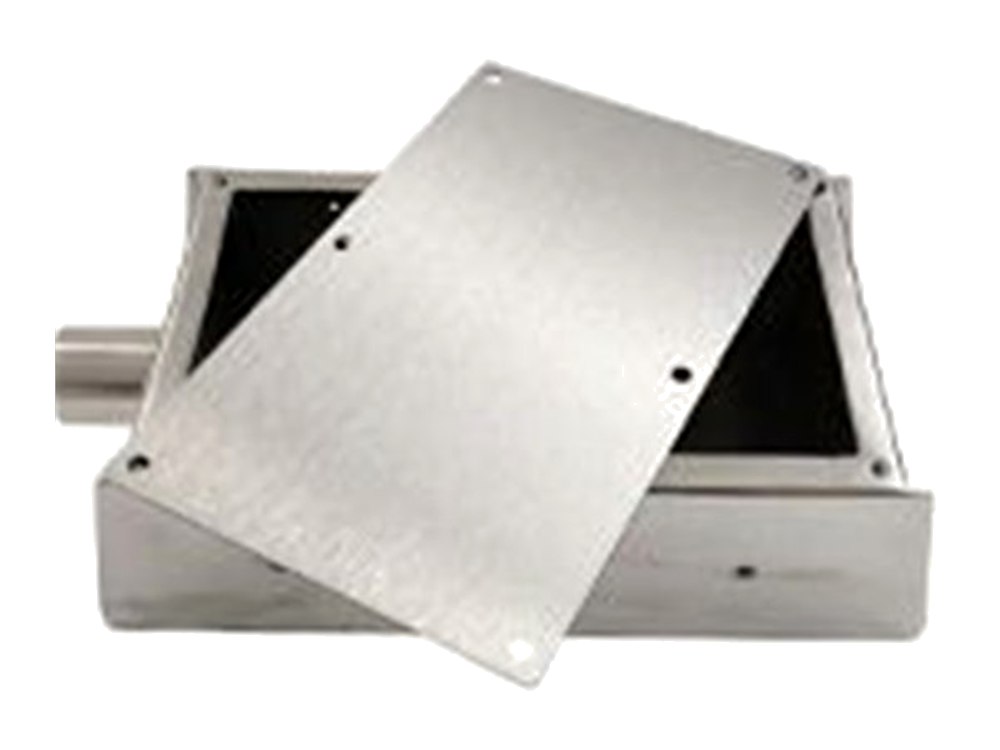
Manufacturing Evidence — Metal Assembly and Sub-Assembly
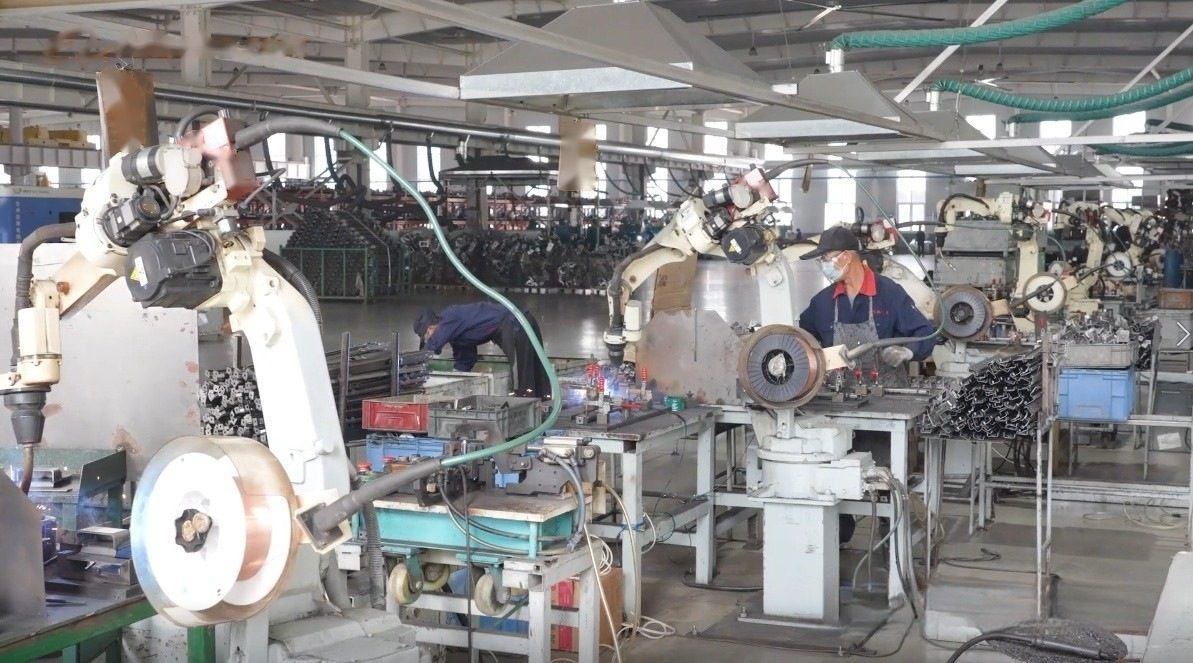
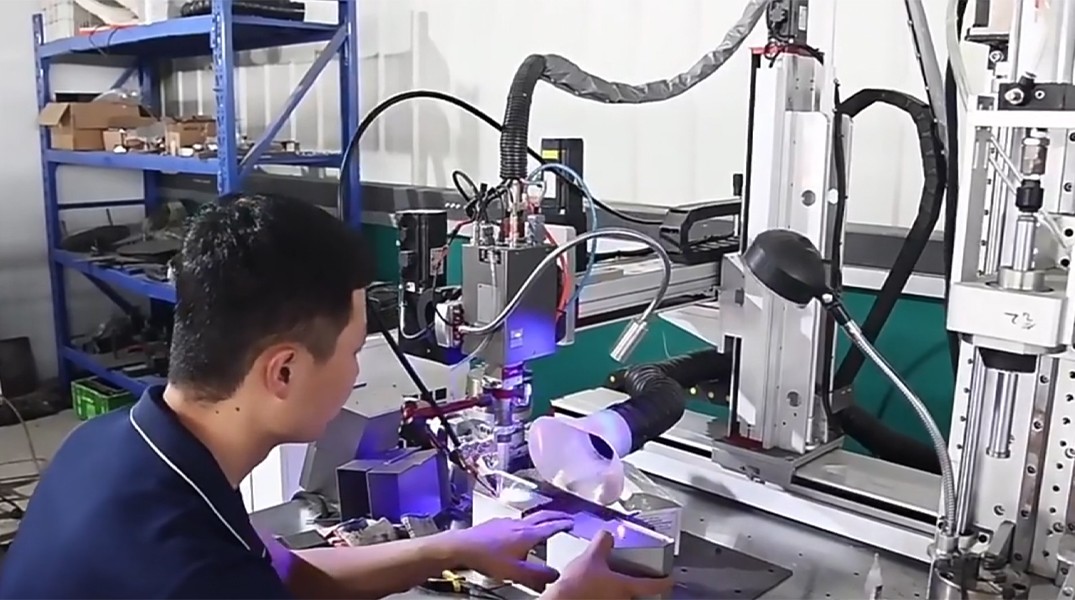
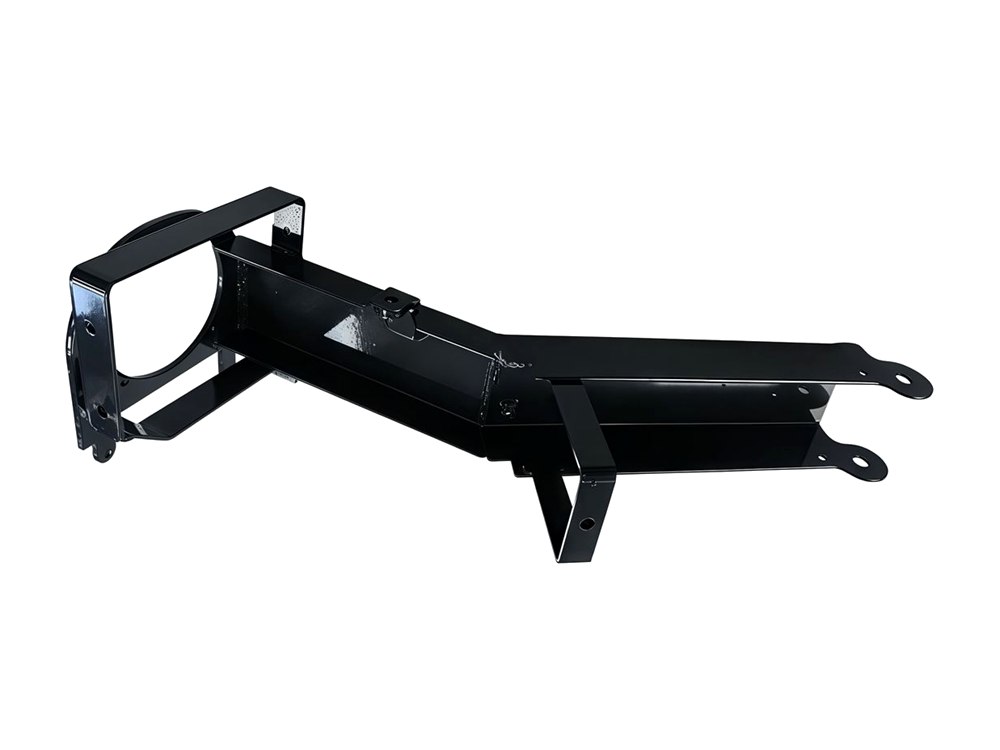
The images below come from the XCWY site asset library and show the plant, equipment, inspection areas and representative parts already published for Metal Assembly and Sub-Assembly.
Frequently Asked Questions
What should I send for a custom metal assembly quotation?
For assemblies, send controlled 2D drawings, available 3D files, revision, material, quantity, finish, hardware or weld notes, critical dimensions, and inspection needs. For assemblies, xCWY offers a quotation response within three business hours when the package is sufficiently defined.
Can XCWY support a one-piece custom metal assembly order?
Yes. The stated MOQ starts from one piece, making custom metal assembly accessible for evaluation or prototype demand. For assemblies, a later production quantity should be requoted because the preferred process and commercial structure may change with volume.
Which materials are available for custom metal assembly?
The listed materials are cold rolled steel, galvanized steel, SS304, SS316, SS316L, AL5052, AL6061-T6, C110 copper, and C260 brass. For assemblies, state the exact grade, thickness or stock form, and condition in the inquiry so XCWY can review process fit without assuming an unspecified substitute.
Which certifications apply to XCWY custom metal assembly?
For assemblies, xCWY lists ISO 9001:2015 registration 34025Q30296R0S. For assemblies, it does not claim ISO 13485, IATF 16949, AS9100, or UL, so buyers whose contracts require those credentials should evaluate that boundary before sourcing.
Can XCWY inspect critical custom metal assembly dimensions?
CMM inspection capability is available. For assemblies, provide the critical characteristics, datums, tolerances, sampling expectation, and reporting requirement so the team can confirm an appropriate method for the specific geometry and surface condition.
Is confidentiality available for a custom metal assembly project?
For assemblies, an NDA is available on request. For assemblies, ask for it before transmitting sensitive files, then keep drawing numbers and revisions consistent across the quotation, technical clarification, order, and any approved change to the project definition.
Continue the Engineering Review
Get a Manufacturing Review and Quote
Attach the drawing, revision, material, quantity, critical tolerances, finish and target date. The inquiry is saved in the site database and emailed to the XCWY team.