 LOADING
Prefer to send a drawing? Use the full RFQ form, email xcwystamping@xcwybj.com or message WhatsApp.
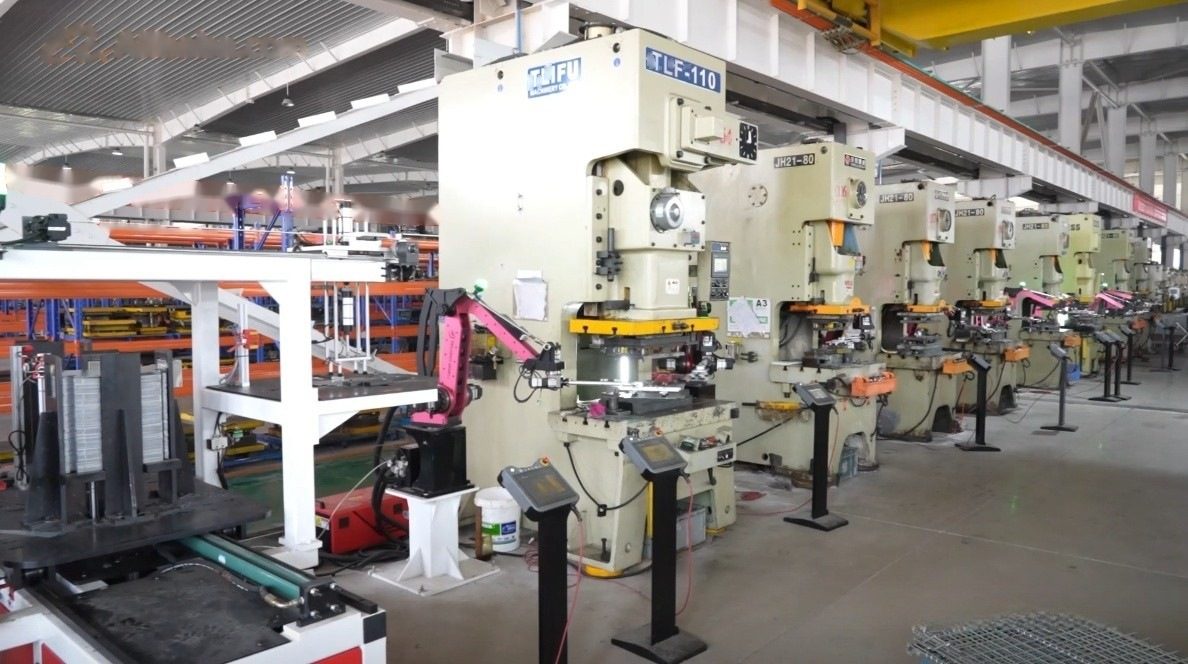
All images below are existing XCWY assets from the factory, production equipment, quality areas or representative custom parts.
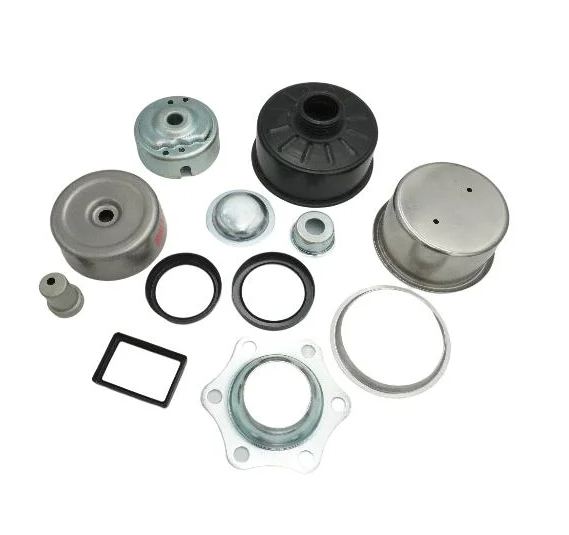
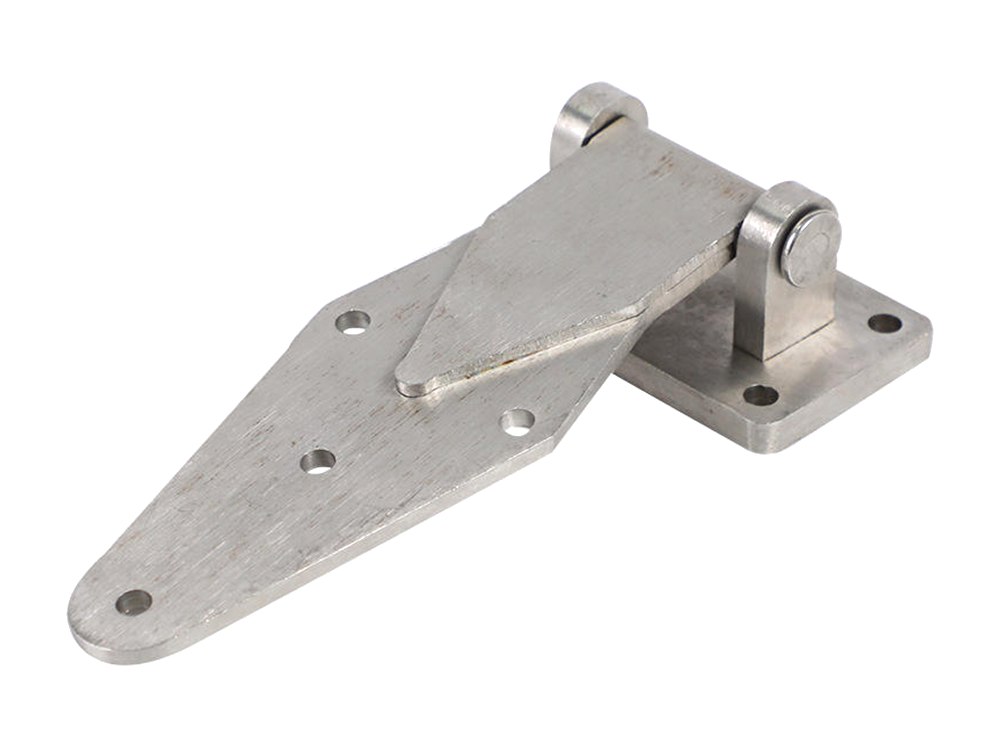
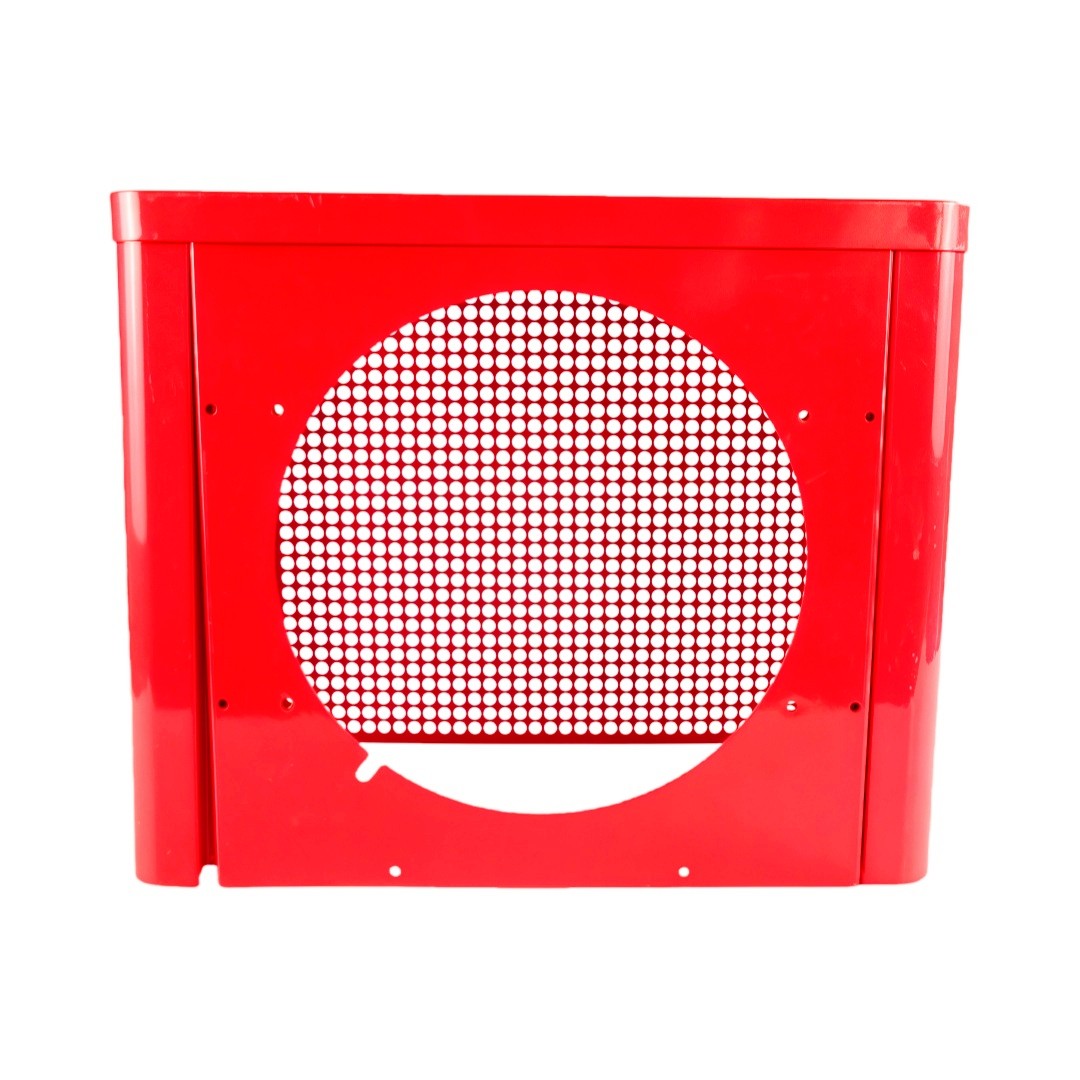
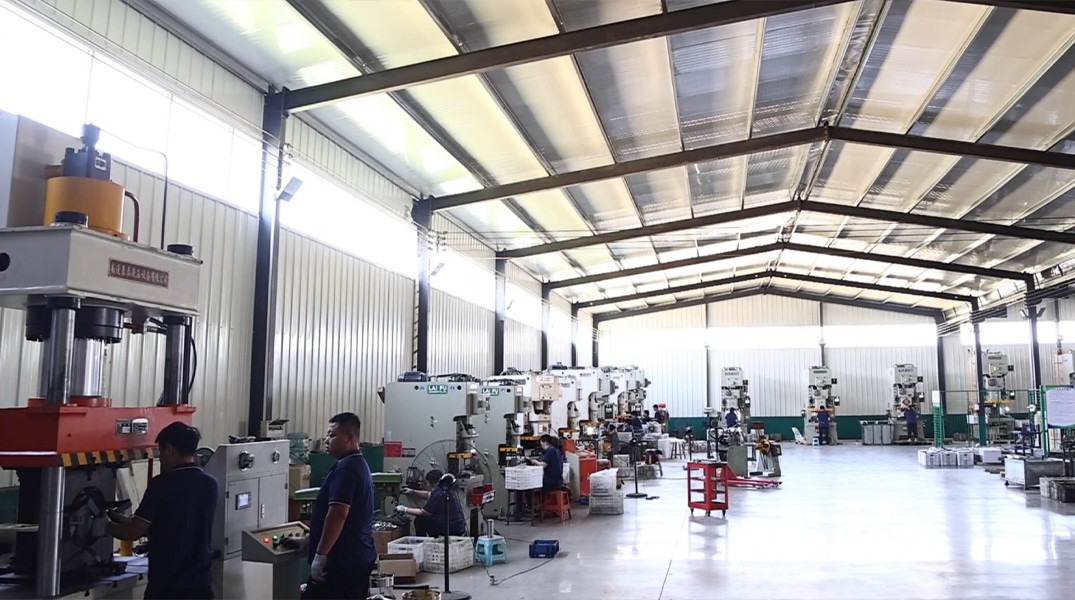
Include material, thickness, quantity, critical dimensions, finish and target date. We will review the manufacturing route before quoting.
Structural platforms for your equipment
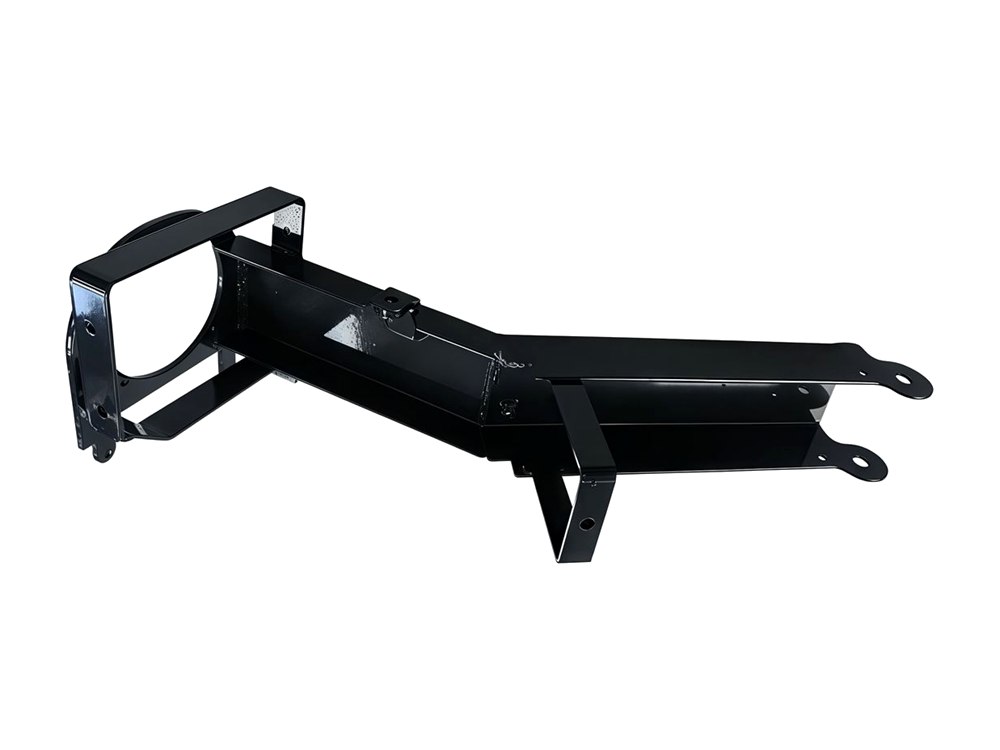
The structure everything else bolts to. Chassis, base frames, sub-assemblies and mounting platforms where hole position, flatness and squareness decide whether your equipment assembles correctly.
A chassis is a reference structure. We agree the datum scheme with you first, then build fixtures around it, so every mounting hole is positioned from the same reference rather than accumulating error panel to panel.
Formed and welded chassis can go straight onto the HDL-OKK DMU38 for precision bores, bosses and datum faces. No shipping a weldment across town and waiting a week for machining.
Welding a chassis moves it. Weld sequence, fixture design and post-weld machining allowances are planned so the finished structure lands inside tolerance.
| Common materials | Cold rolled steel, hot rolled plate, AL5052, AL6061-T6 |
| Sheet and plate range | 1.2 – 6.0 mm typical; heavier plate by arrangement |
| Forming | CNC press brake ±0.5°, up to 3,200 mm |
| Welding | MIG, TIG and laser welding with fixture control |
| Machining | Simultaneous 5-axis, HDL-OKK DMU38, ±0.005 mm |
| Assembly tolerance | Typically ±0.5 mm on welded structures, tighter where machined |
| Quality basis | ISO 9001:2015 · registration 34025Q30296R0S |
Yes, and it is usually the right sequence. Welding moves the structure, so critical bores, bosses and mounting faces are machined after welding on the HDL-OKK DMU38 with material allowance planned in from the start.
It depends on size, gauge and whether the surface is machined. As-fabricated flatness is typically controlled to the drawing tolerance for the panel size; machined faces are held far tighter. Give us the functional requirement and we will confirm what is achievable before quoting.
5052 forms well and suits bent chassis and enclosure-style structures. 6061-T6 is stronger and machines cleanly but cracks at tight bend radii. Many chassis use both — formed panels in 5052, machined brackets in 6061-T6.
Yes. PEM inserts, threaded bosses, standoffs and mounting hardware are fitted in-house, and sub-assemblies can be built up before shipment.
Every order ships with a first-article dimensional report. For chassis with machined features, CMM verification of critical dimensions is included.
Laser-cut and formed chassis without tooling typically move fastest since no dies are required. Send the model and we return lead time with the quote inside three business hours.