 LOADING
Prefer to send a drawing? Use the full RFQ form, email xcwystamping@xcwybj.com or message WhatsApp.
Built for mud, weather and impact
Custom agricultural equipment fabrication: structural brackets, guards, hoppers, panels and welded frames in heavy-gauge steel — specified for outdoor exposure, abrasive contact and vibration loading farm machinery actually sees.
Agricultural equipment lives outdoors under vibration, impact and abrasive contact. Gauge selection, weld sizing and coating are chosen for that reality rather than for the lowest quote.
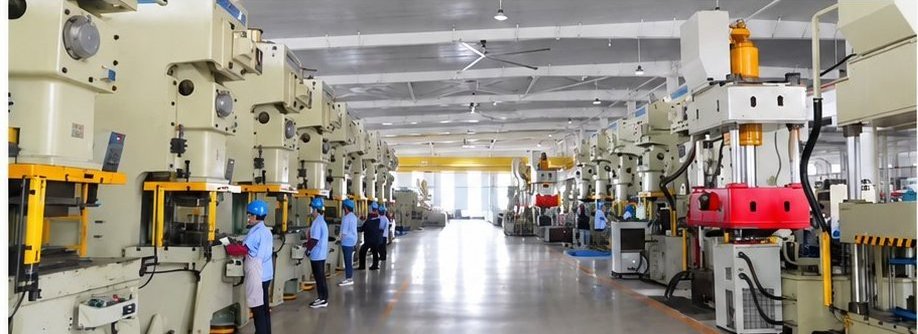
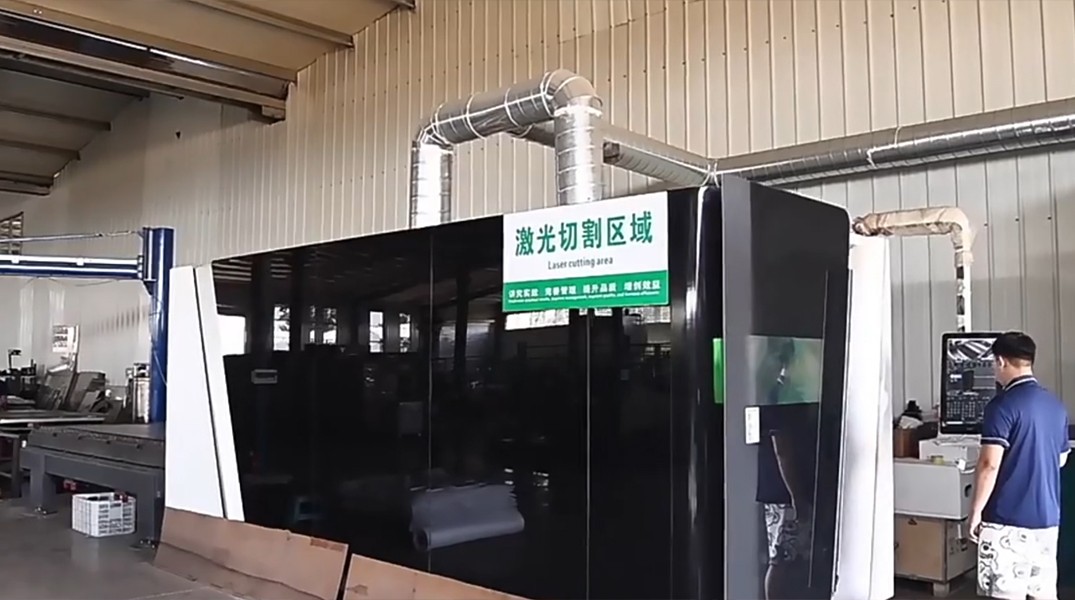
Our 400-ton press capacity and 25 mm laser cutting range cover the heavier sections agricultural work needs. Thicker material means larger bend radii and different weld preparation — planned in, not discovered.
Powder coating over galvanized steel gives the best combination of corrosion resistance and impact tolerance for equipment that will be pressure-washed and knocked about.
| Primary materials | Hot rolled steel, cold rolled steel, galvanized steel, SS304 |
| Thickness range | 1.5 – 6.0 mm production; laser cutting to 25 mm carbon steel |
| Press capacity | Up to 400 ton for heavy stamped sections |
| Welding | MIG for structural joints, TIG where finish matters |
| Forming | CNC press brake to 3,200 mm with heavy-gauge tooling |
| Finishing | Powder coating, hot-dip compatible galvanized base material, zinc plating |
| Quality basis | ISO 9001:2015 · registration 34025Q30296R0S |
Production forming runs to 6.0 mm, with laser cutting up to 25 mm on carbon steel for heavy plate components. Our 400-ton press capacity covers heavy stamped sections.
We fabricate from galvanized base material and apply powder coating in-house. For post-fabrication hot-dip galvanizing on completed weldments, tell us at RFQ so it is coordinated and priced into the lead time.
Powder coating over galvanized steel gives the best balance — 500–1,000+ hours neutral salt spray plus impact tolerance. Zinc plating alone is not suitable for equipment that lives outdoors.
Yes. MIG welding handles structural thickness efficiently, with fixture-controlled sequences to manage distortion and post-weld dimensional verification before coating.
Yes. Send the physical part and we can reverse-engineer it to a drawing, then confirm material, tolerance and finish with you before production. A drawing is faster and more accurate, but a sample works.
Production orders can start from a single piece. Prototype and first-article parts are produced from a single unit, which is worth doing on structural parts before committing to a batch.
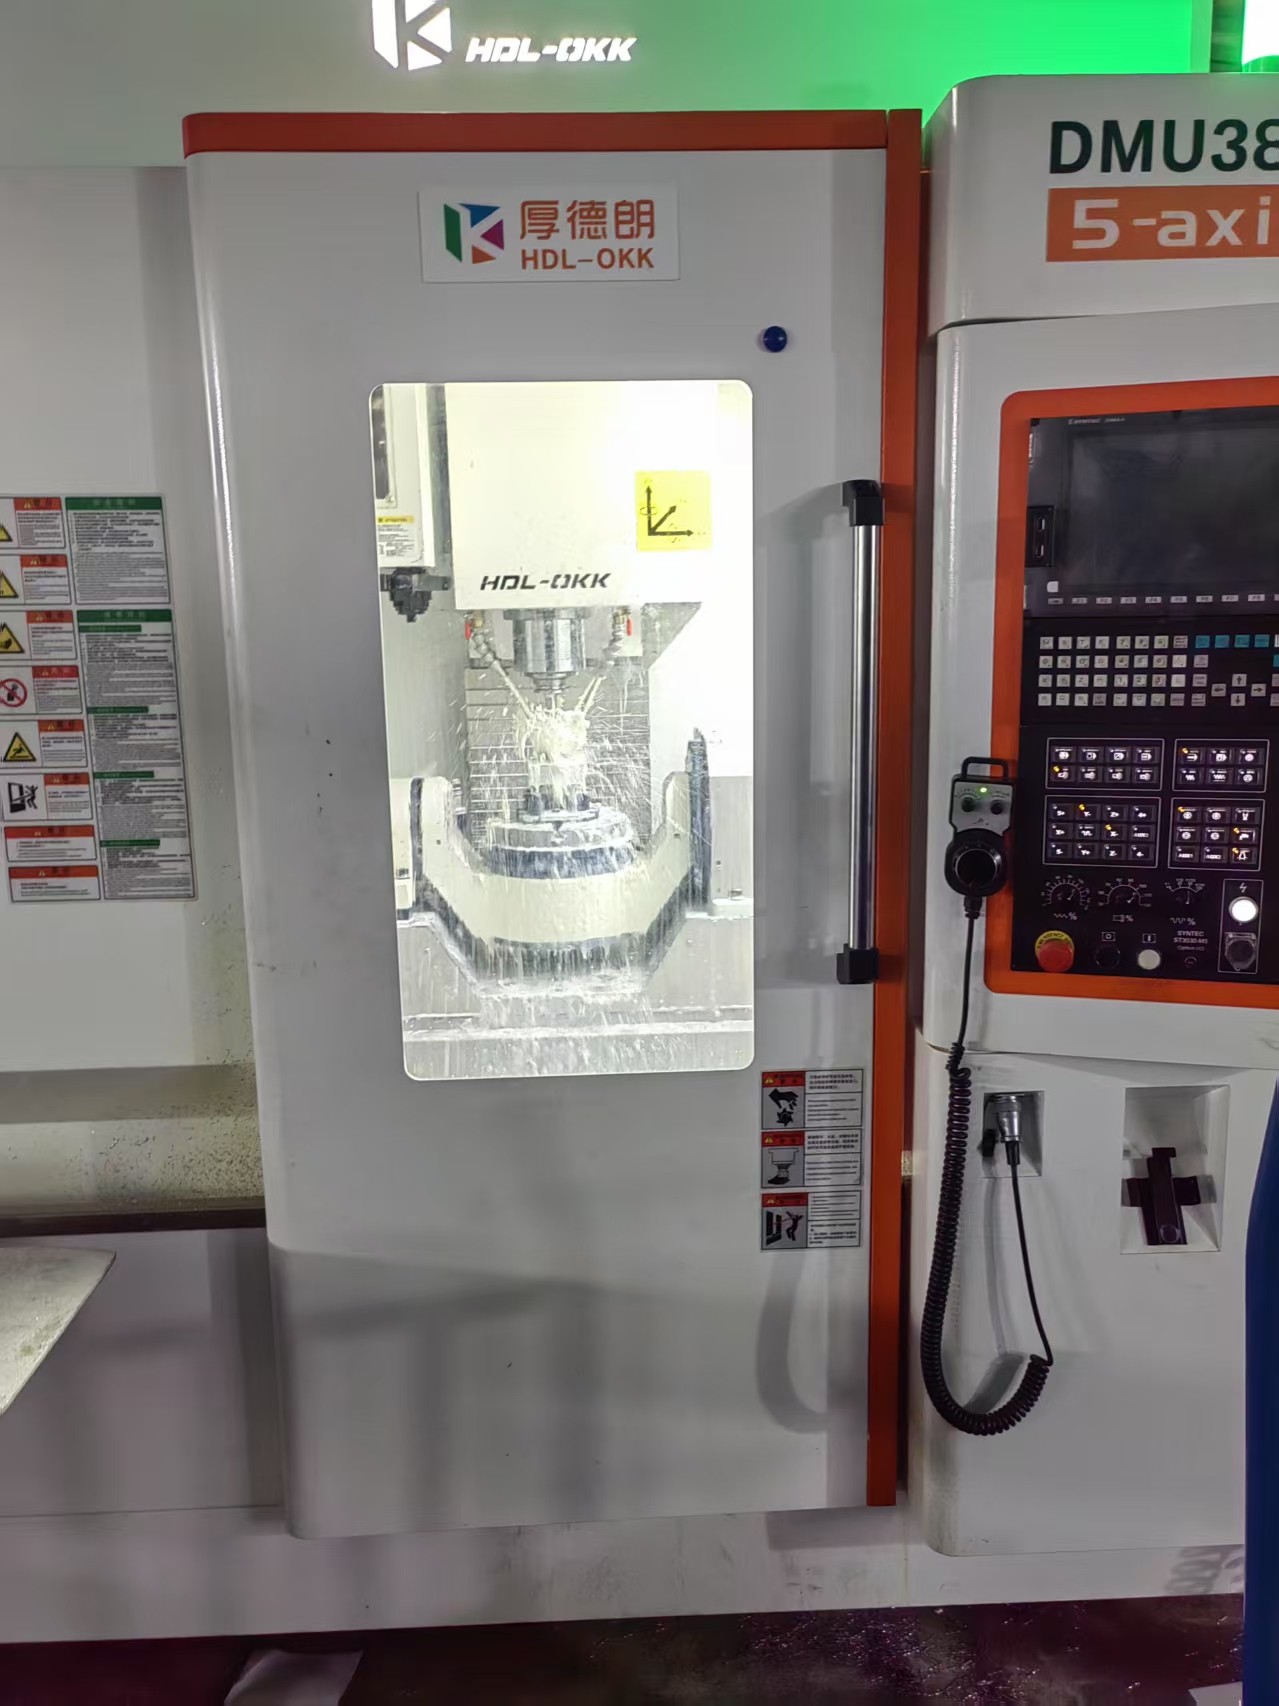
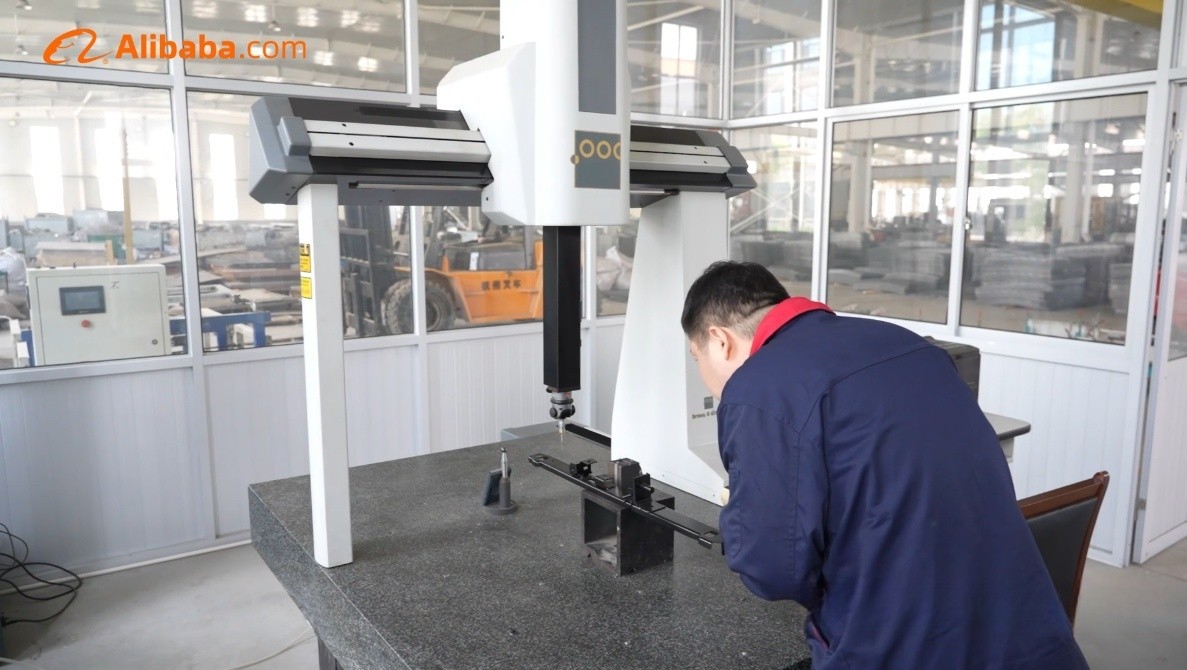
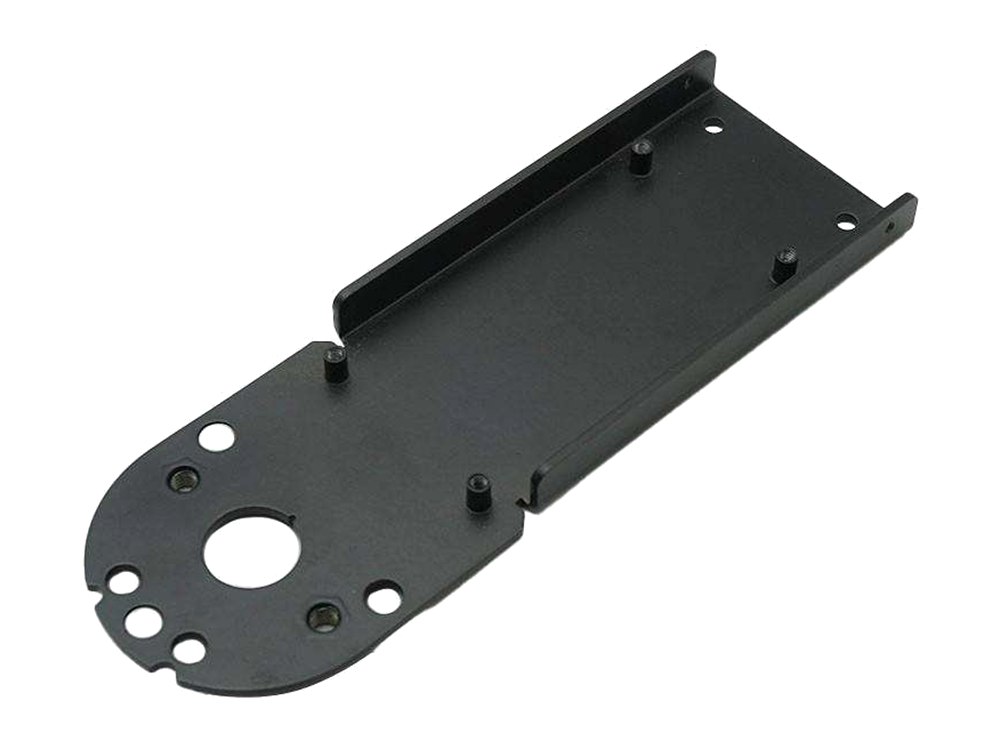
All images below are existing XCWY assets from the factory, production equipment, quality areas or representative custom parts.
Include material, thickness, quantity, critical dimensions, finish and target date. We will review the manufacturing route before quoting.