 LOADING
Prefer to send a drawing? Use the full RFQ form, email xcwystamping@xcwybj.com or message WhatsApp.
Built for programme discipline
Custom EV battery housing and automotive metal parts: battery module trays, copper busbar, structural brackets and high-volume metal stampings produced under documented process control, with PPAP documentation where your supplier quality manual requires it.
Automotive programmes run for years. Fixtures, weld sequences, control plans and inspection points are documented at first article so batch fifty matches batch one — which is the entire point of a production supplier.
Busbar and battery interconnects in C110 copper need sharp tooling and correct lubrication because copper is gummy and smears. Aluminium battery trays need weld distortion control. Different metals, different discipline.
XCWY holds ISO 9001:2015. We are not IATF 16949 certified. We supply PPAP documentation packages and run to your control plan, but if your programme mandates an IATF-certified supplier, confirm that requirement before qualification starts.
| Primary materials | CRS, galvanized steel, AL5052, AL6061-T6, C110 copper, 65Mn spring steel |
| Typical processes | Progressive stamping, deep drawing, laser cutting, welding, machining |
| Stamping tolerance | ±0.05 mm on critical features |
| Documentation | PPAP Level 3 available: PFMEA, control plan, MSA, dimensional results |
| Press capacity | 25 – 400 ton |
| Certification held | ISO 9001:2015 · 34025Q30296R0S (not IATF 16949) |
No. We hold ISO 9001:2015, registration 34025Q30296R0S. We supply PPAP Level 3 documentation and run production to your control plan, but we are not IATF 16949 certified. If your programme requires an IATF-certified tier supplier, please confirm that at RFQ.
Process flow diagrams, PFMEA, control plans, MSA, dimensional results, material certifications and appearance approval reports. Level 3 is our standard for automotive customers; other levels are supported per your supplier quality manual.
Yes. C110 copper is laser cut with nitrogen assist for oxide-free edges, then formed, and plated where specified. Copper machines and stamps differently from steel, so tooling and lubrication are set up specifically for it.
Fixture design, staggered tacking, weld sequence planning and choosing the lowest-heat process that satisfies the joint — often laser welding rather than MIG on thinner sections. Post-weld dimensions are verified before release.
Statistical process control is run where your control plan specifies it. Tell us which characteristics require SPC and the capability targets, and they are built into the control plan at first article.
Progressive dies typically make sense from around 50,000 pieces per year upward. Between roughly 10,000 and 500,000, compound tooling is often the better economic fit. We quote the alternatives so the crossover is visible.
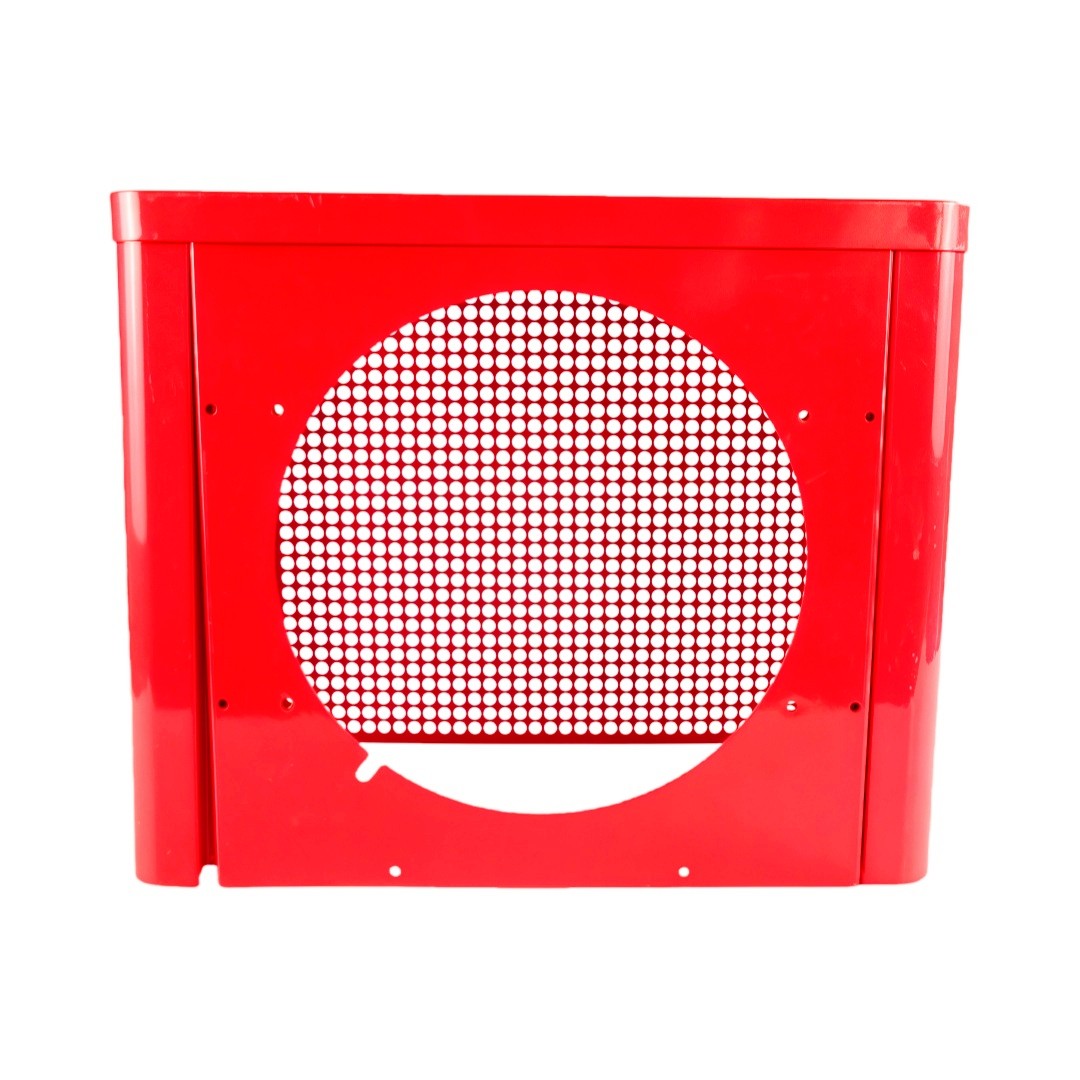
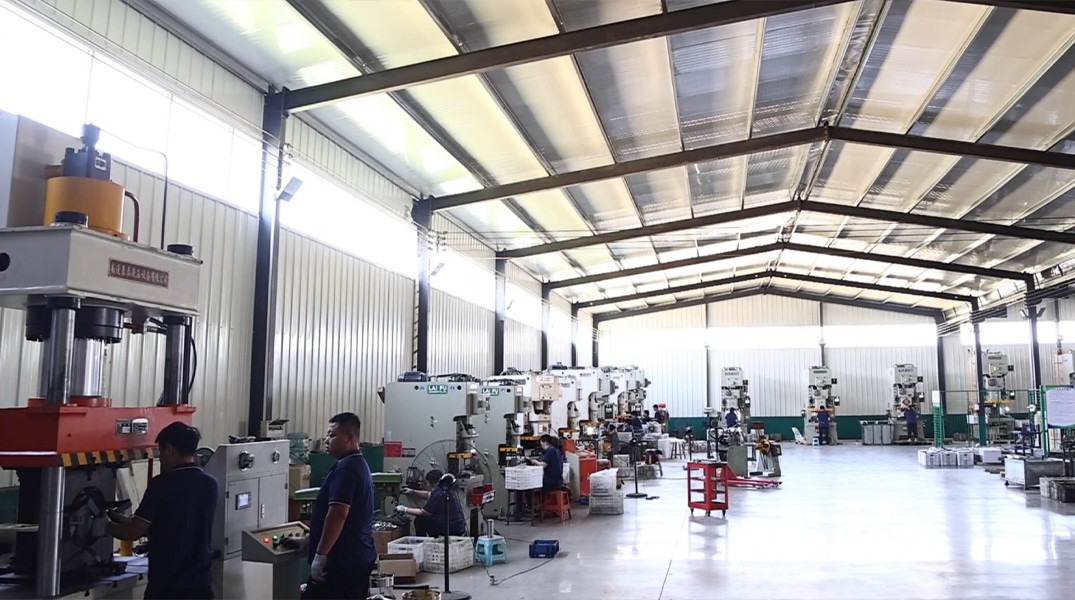
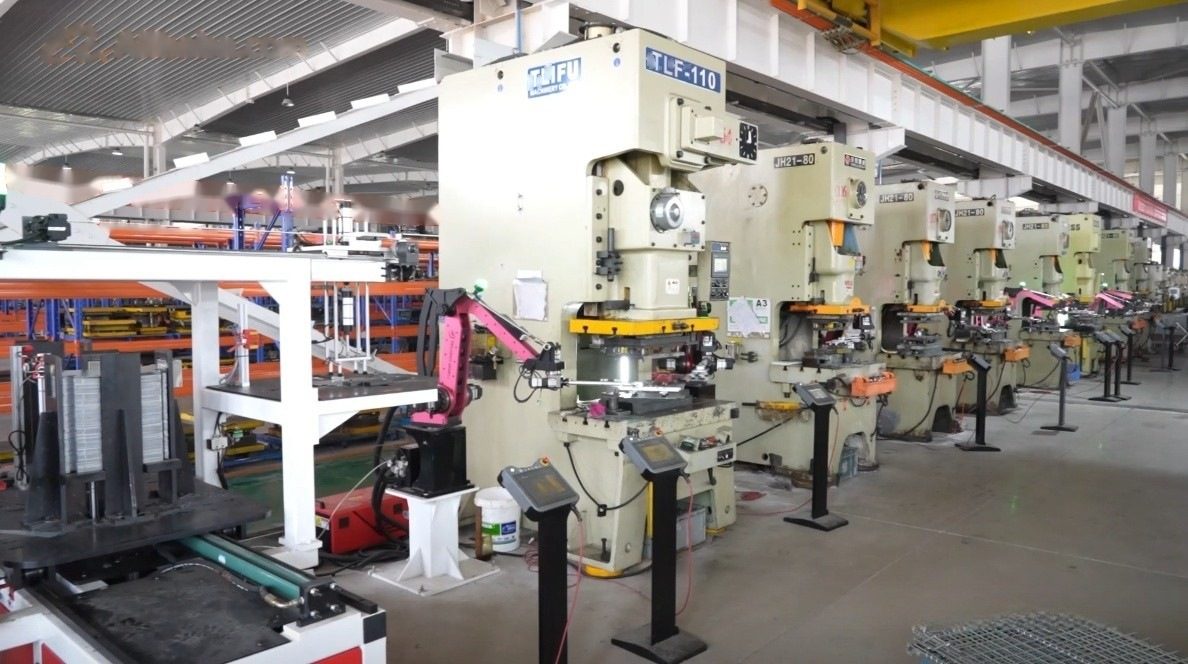
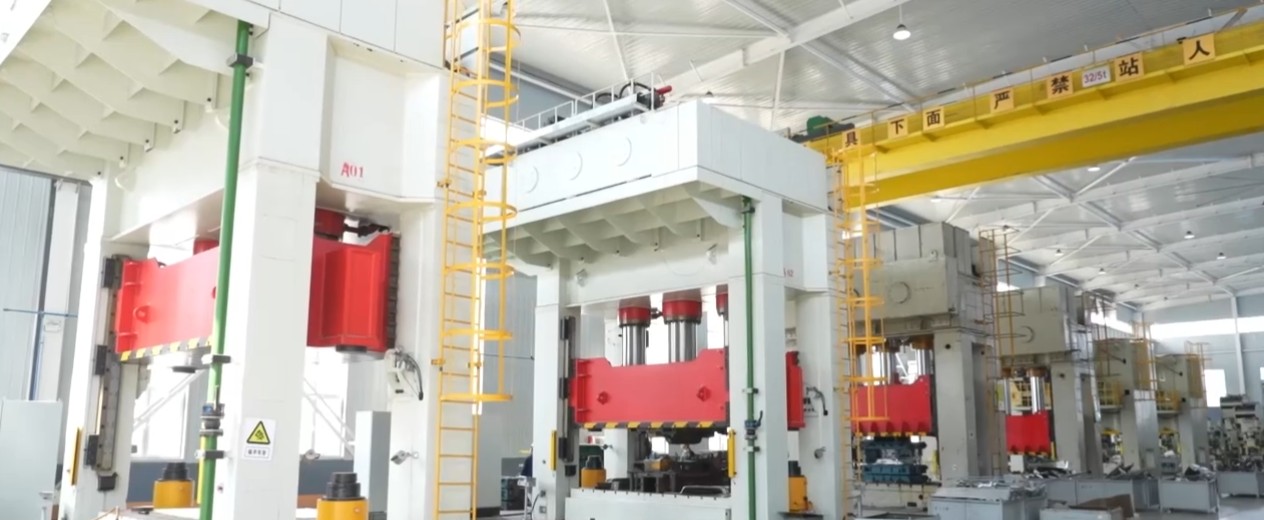
All images below are existing XCWY assets from the factory, production equipment, quality areas or representative custom parts.
Include material, thickness, quantity, critical dimensions, finish and target date. We will review the manufacturing route before quoting.