Custom Progressive Stamped Brackets
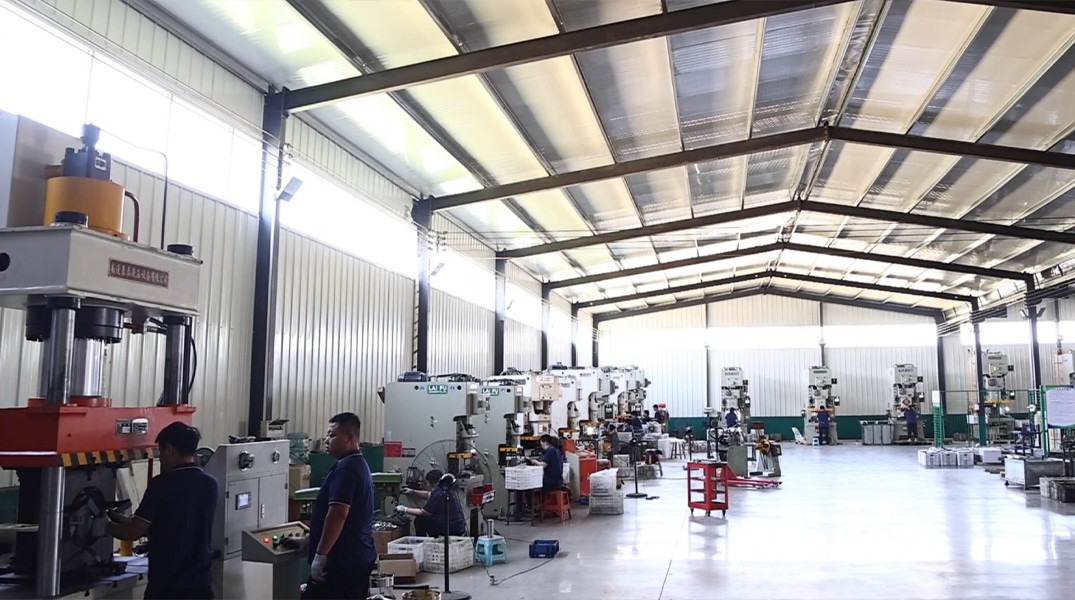
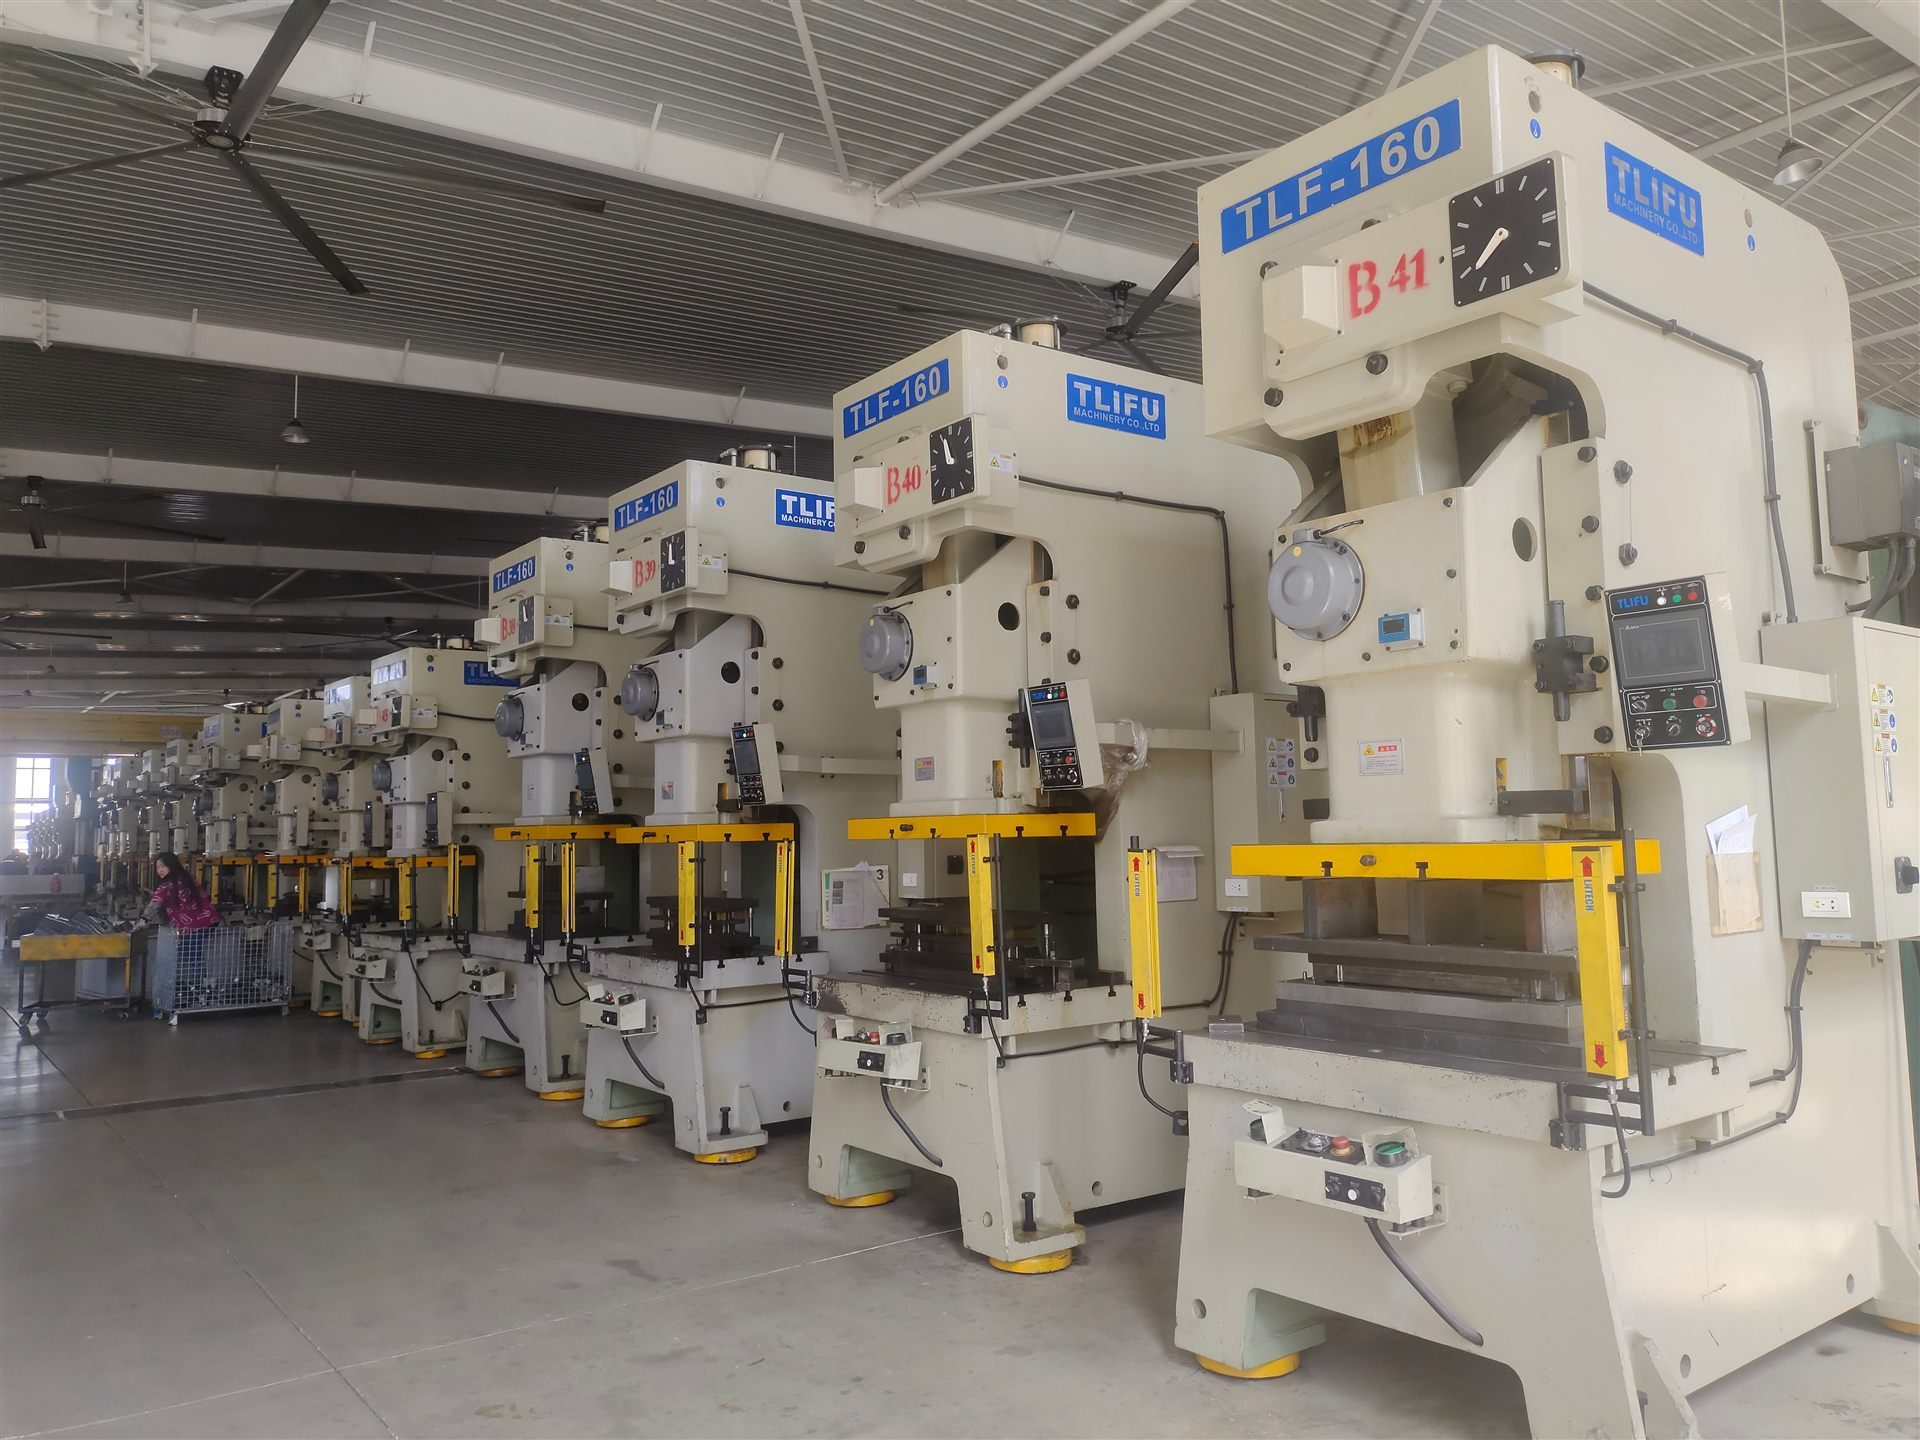
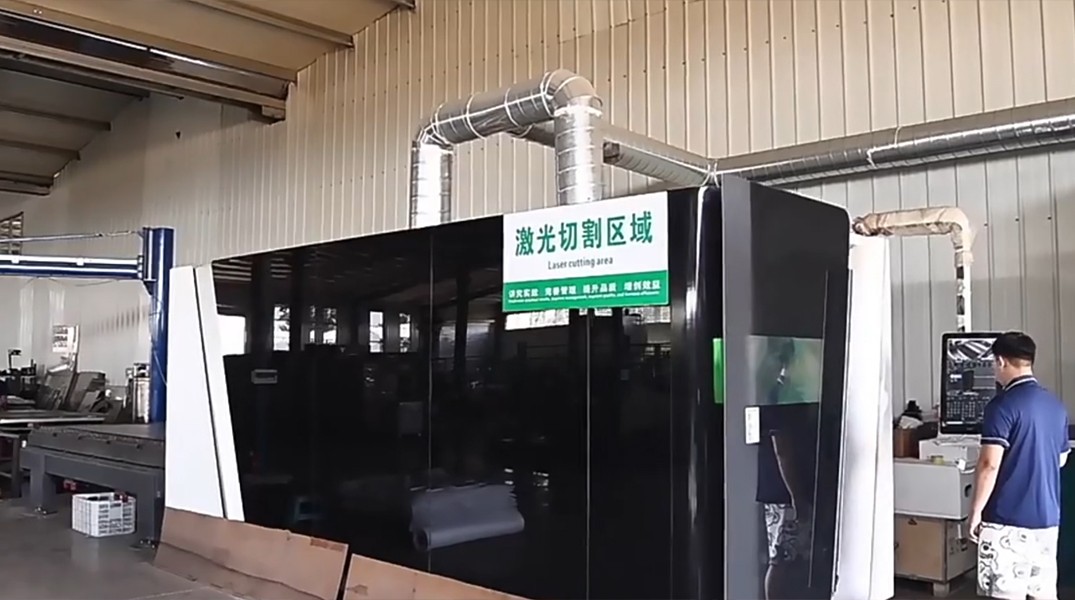
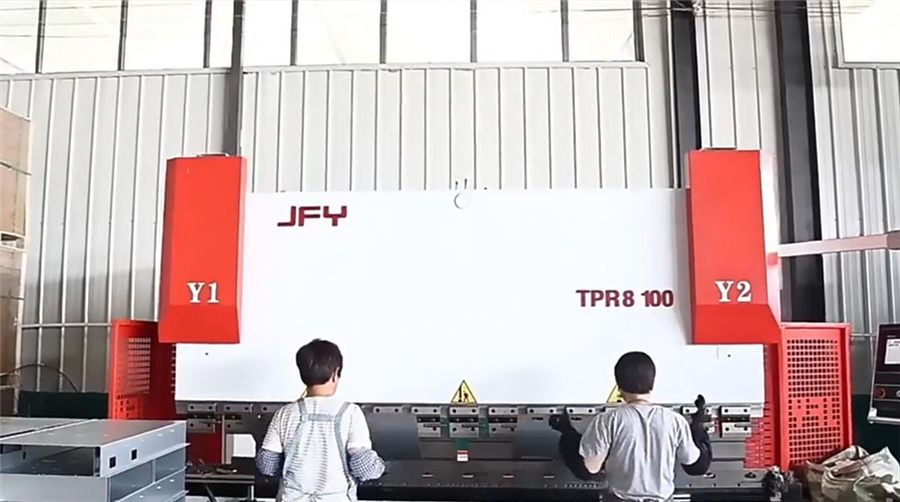
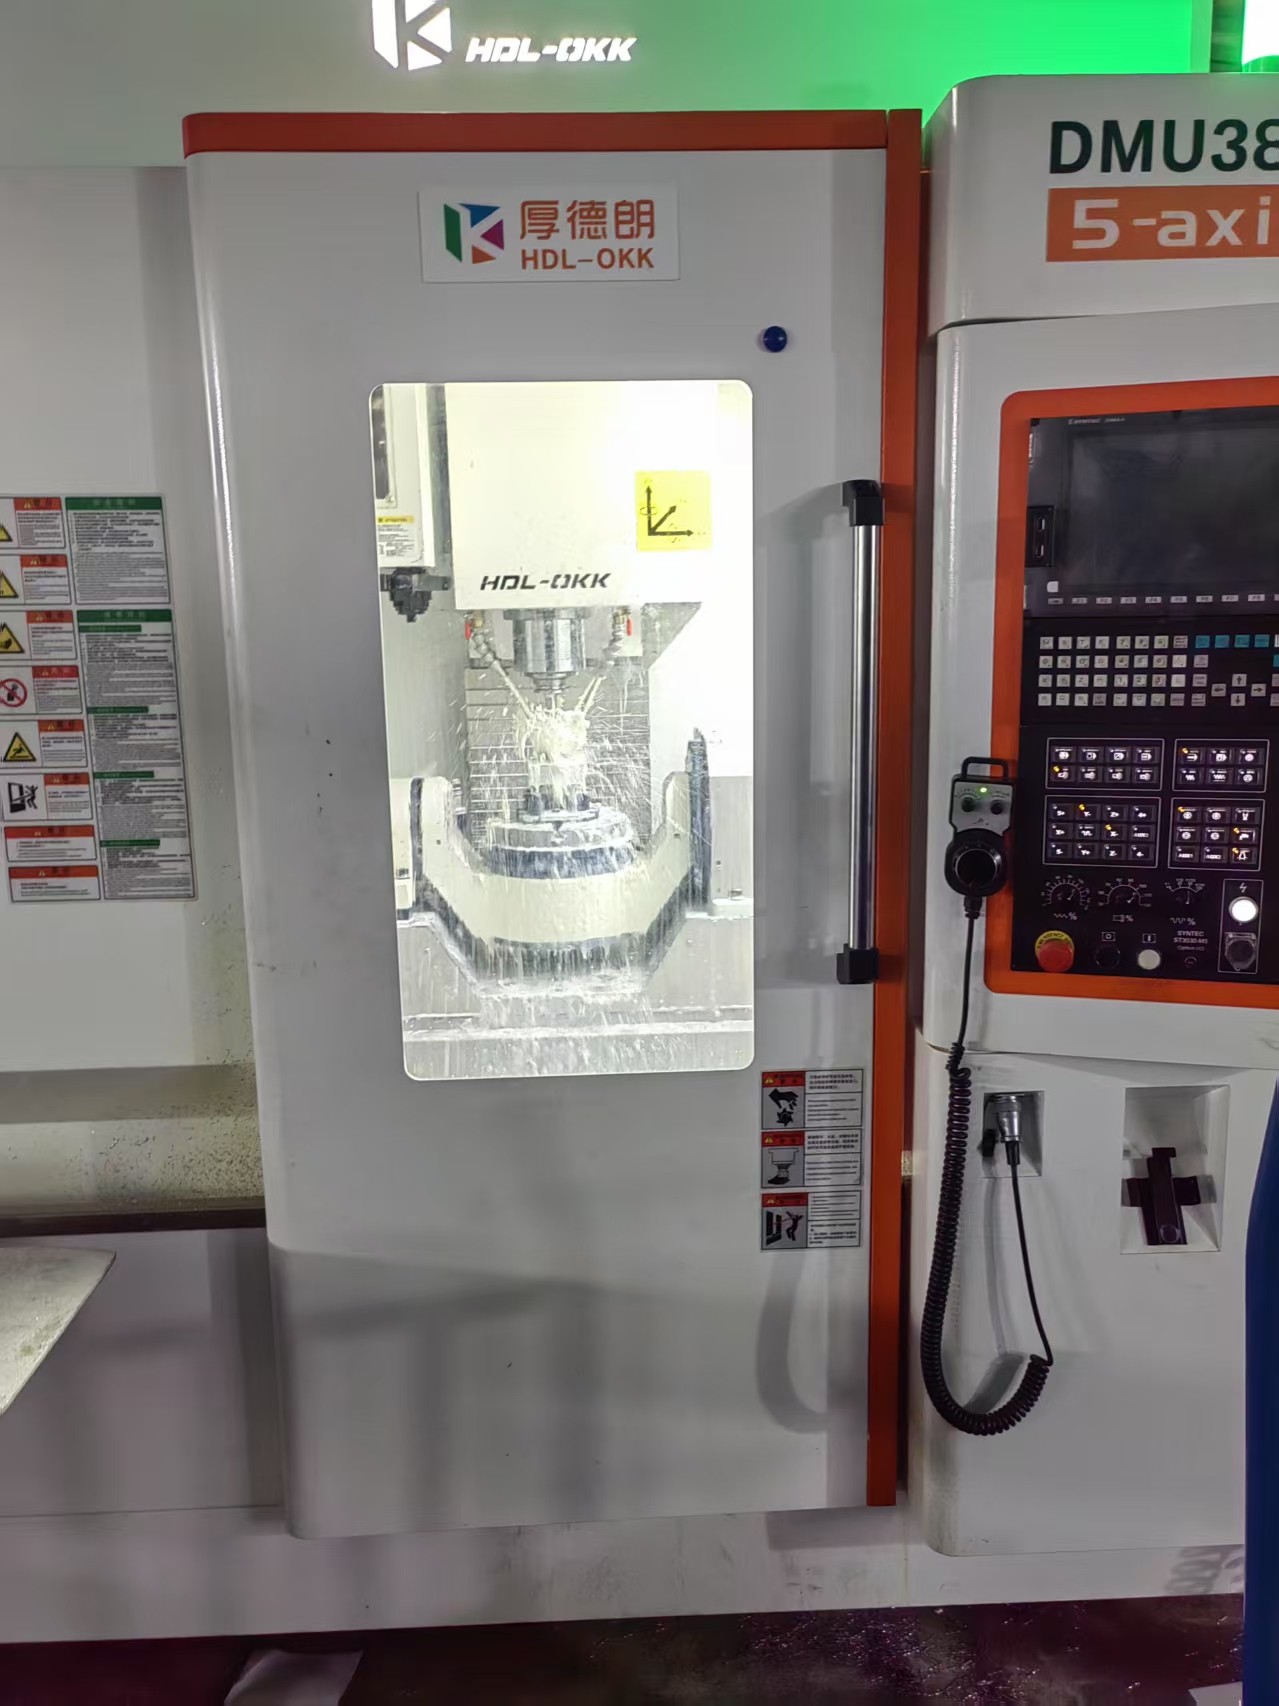
XCWY supports buyers developing custom parts with drawing-based metal manufacturing and practical engineering review. Founded in 1998, the factory operates in a 15,000 m² facility with six production lines and 78 staff. Available processes include 25–400T pressing, 12kW laser cutting, precision press-brake forming, five-axis machining, laser/TIG/MIG/spot welding, and PEM insertion. The 12kW laser cuts carbon steel to 25 mm, stainless steel to 20 mm, aluminum to 12 mm, and copper to 6 mm. A 3,200 mm press brake works to ±0.5° angle capability, while five-axis machining reaches ±0.005 mm under suitable conditions. CMM inspection supports dimensional verification. ISO 9001:2015 registration 34025Q30296R0S covers the quality system. MOQ starts at one piece, NDA handling is available, and complete RFQs are targeted for quotation within three business hours. This page explains scope, choices, risks, and the information needed for a defensible manufacturing route.
Request a Drawing Review
Attach the drawing, revision, material, quantity, critical tolerances, finish and target date. The inquiry is saved in the site database and emailed to the XCWY team.
Design Scope
A useful engineering program begins by defining the real component family rather than requesting a generic metal part. Typical scope includes mounting brackets, retaining clips, connector supports, spring tabs, grounding contacts, reinforcement plates, cable guides, and multi-bend hardware produced through sequenced die stations. Each item carries different load paths, access needs, appearance zones, and production volumes, so XCWY reviews the assembly context before proposing a process. Important interfaces commonly include strip carrier, pilot holes, station pitch, bend sequence, coined areas, pierced features, cutoff edge, formed tabs, and assembly datums. These features should be dimensioned from stable datums instead of accumulated edge chains. A 3D model helps visualize the assembly, but a revision-controlled 2D drawing remains essential for tolerances, material, finish, burr direction, and inspection notes. Early DFM examines bend relief, inside radii, hole-to-edge distance, tool approach, weld access, hardware installation, and realistic measurement points. Prototype quantities may favor laser cutting and brake forming, while repeat demand can justify hard tooling or progressive operations. Machining is reserved for features that truly need it. XCWY does not assume service loads, environmental class, or legal compliance on the buyer’s behalf. Buyers should provide mating-part data, critical load cases, restricted substances, and any governing standards. That shared definition keeps design responsibility visible, reduces quotation ambiguity, and prevents a low-cost process choice from creating expensive assembly problems later.
Materials and Surface Decisions
Material selection should connect mechanical function, fabrication behavior, corrosion exposure, appearance, and supply condition. XCWY can process CRS, galvanized steel, SS304, AL5052, C110, C260, and 65Mn selected for formability, strength, conductivity, spring performance, and strip availability; SS316L and AL6061 are reviewed case by case. A grade name alone is not enough: thickness, temper or hardness, applicable standard, grain limits, and certificate expectations should appear in the RFQ. Substitution is not made silently because strength, elongation, conductivity, bend response, weldability, and coating adhesion can change. Surface choices include zinc plating, powder coating, passivation, anodizing, brushing, or polishing arranged after stamping when required, with rack or barrel effects and dimensional buildup considered. The drawing should state the process, color or appearance, thickness or class where relevant, masking locations, and cosmetic acceptance zones. Threads, PEM interfaces, grounding points, gasket lands, press fits, and weld areas may require protection from finish buildup. Mixed metals also need review for galvanic risk, especially where moisture can remain. Forming direction and visible grain matter for brushed or polished surfaces, while rack marks and contact points must be assigned to noncritical areas when possible. Finish approval can use a customer standard, measurable specification, or signed sample rather than subjective words such as “good” or “smooth.” Material certificates and finish certificates can be included when requested and defined. These decisions allow sourcing, tooling, forming, welding, and inspection teams to work from the same technical baseline.
Manufacturing Route and Capacity
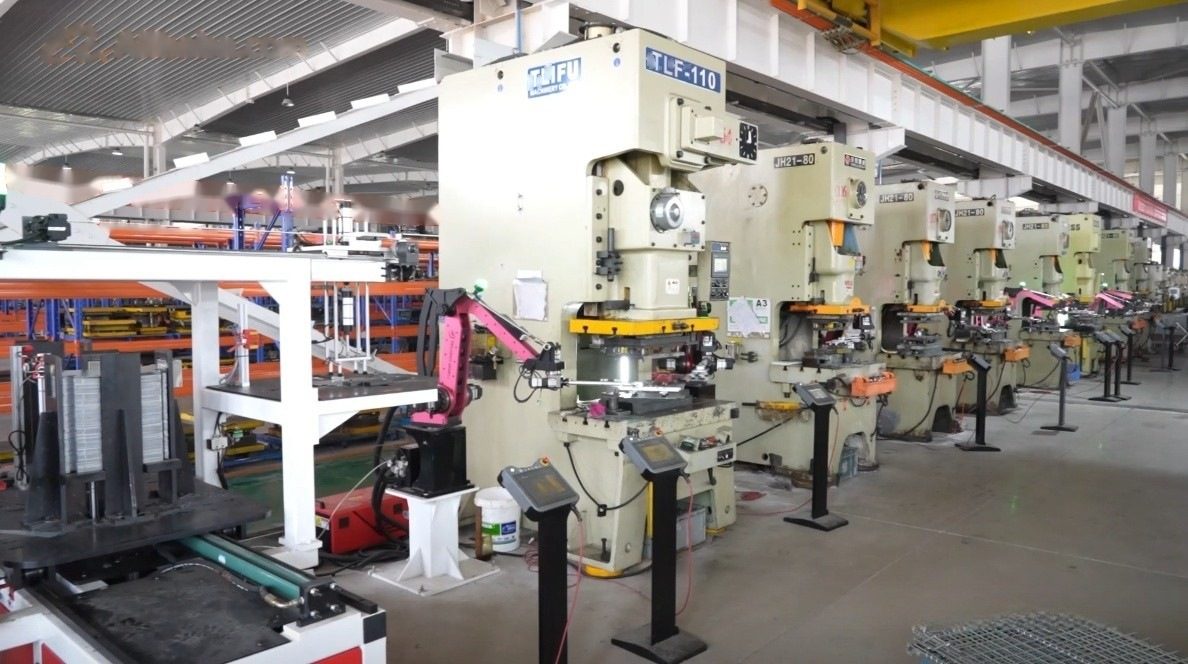
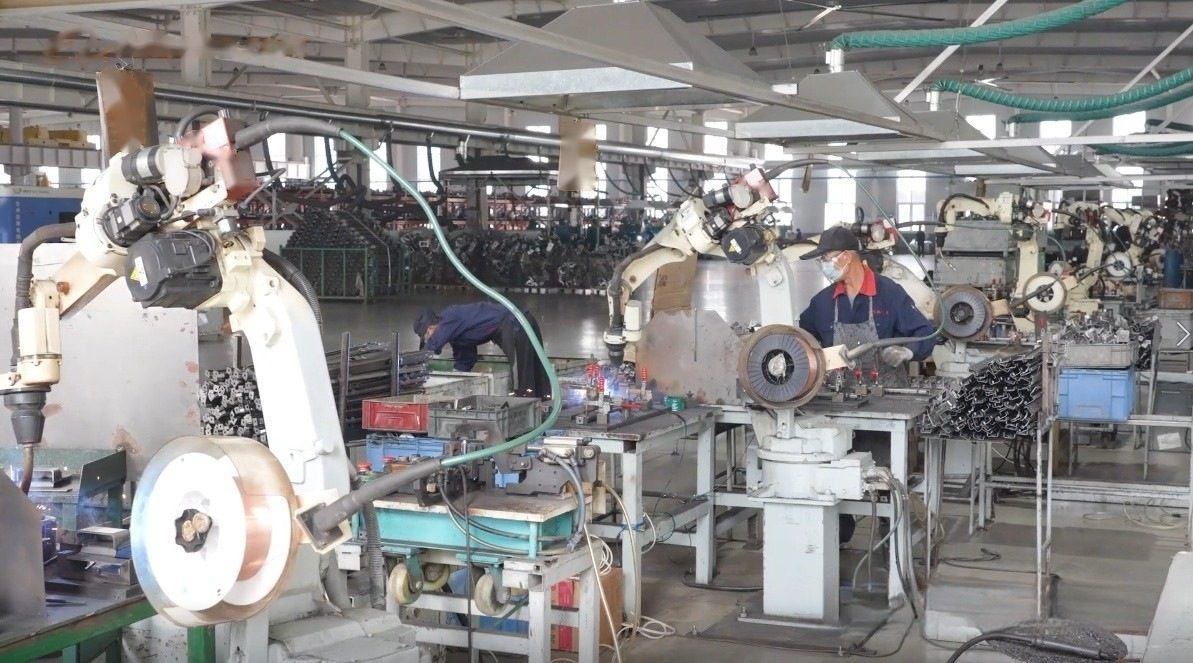
XCWY selects the manufacturing route from geometry, volume, tolerance, material, and finish rather than forcing every design through one machine. Six production lines combine presses from 25 to 400T with a 12kW laser, a 3,200 mm press brake, five-axis machining, welding, hardware insertion, and inspection. The laser has stated cutting limits of 25 mm carbon steel, 20 mm stainless steel, 12 mm aluminum, and 6 mm copper; actual edge quality and speed still depend on grade, thickness, geometry, gas, and acceptance criteria. The brake provides ±0.5° angle capability under appropriate setup, while five-axis machining can reach ±0.005 mm where part shape, fixturing, material stability, and measurement method support it. Prototype blanks can validate fit before tooling investment. Higher volumes may move to compound, transfer, or progressive stamping after demand and tool economics are confirmed. Laser, TIG, MIG, and spot welding are available, with sequence and fixturing planned to limit distortion. PEM insertion can consolidate assembly, but hole preparation, sheet hardness, edge distance, and push-out needs must be specified. Process transitions are documented so that cut parts, formed parts, weldments, inserted hardware, and finished goods remain linked to the correct revision. The resulting route aims for repeatability without claiming that every advertised machine capability applies to every feature.
Quality Planning and Failure Control
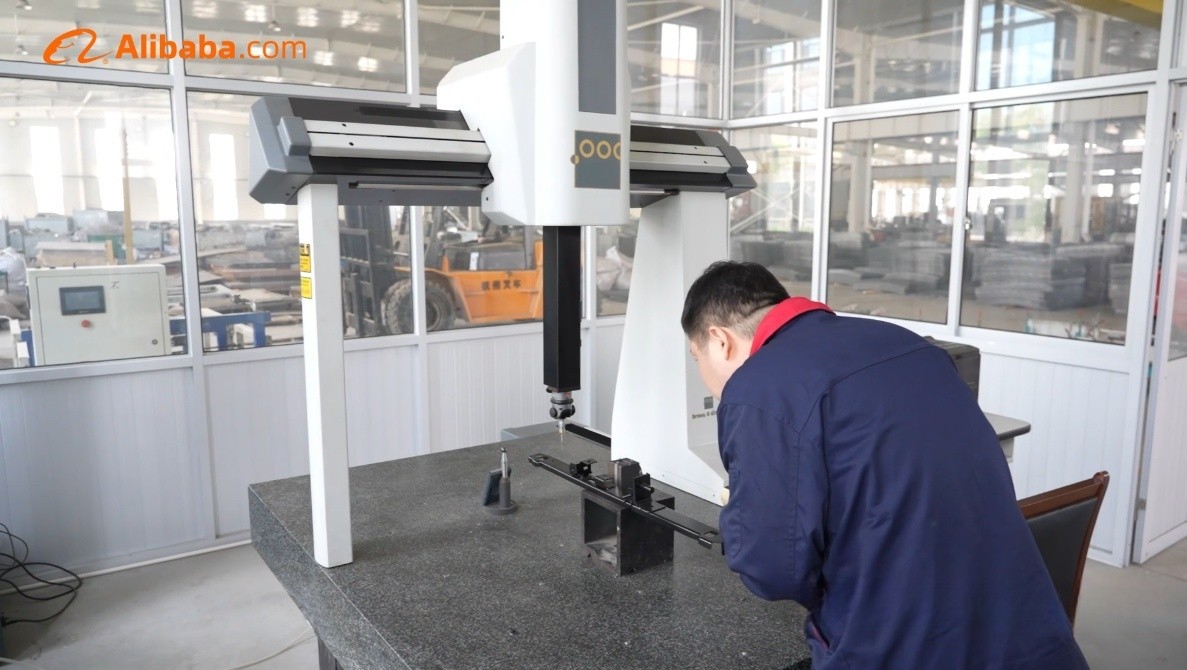
Quality planning starts with likely failures, not with a final inspection checklist. Relevant concerns include progressive pitch error, punch wear, slug pulling, burr growth, carrier distortion, springback, split bends, mixed lots, and coating damage in secondary operations. XCWY reviews which characteristics prevent these outcomes, how those characteristics are produced, and which method can verify them. CMM inspection is available for suitable dimensional features, while dedicated gauges, calibrated hand tools, visual standards, coating tests, fit checks, and functional fixtures may be more appropriate elsewhere. The control plan should identify critical dimensions, sampling level, inspection stage, measurement condition, and reaction path. Welded or formed assemblies need datums that remain stable after processing; flexible edges are poor inspection references. Cosmetic requirements benefit from defined viewing distance, lighting, allowed defect size, and zone classification. Material identity, hardware type, finish batch, and revision status can be captured according to the agreed traceability level. First-article evidence is useful before volume release, and PPAP Level 3 is available when requested, particularly when the customer supplies the required format and submission expectations. XCWY is ISO 9001:2015 registered under 34025Q30296R0S, but it is not IATF, ISO 13485, AS9100, or UL certified. Any sector-specific approval or product certification remains a separately defined customer requirement and must not be inferred from the quality-system certificate.
RFQ, Documentation, and Commercial Handoff
A complete custom parts RFQ shortens review time and produces a more comparable quotation. The preferred package contains released part drawing, annual and lot volumes, material specification, grain or temper requirement, burr direction, finish, critical dimensions, gauge plan, tool ownership terms, and PPAP Level 3 package when requested. Include target quantity, prototype and annual demand, delivery location, desired schedule, and whether tooling is customer-owned. Native CAD plus a readable PDF reduces interpretation risk; conflicting dimensions or revisions should be resolved before release. XCWY targets a quotation within three business hours after receiving complete information, although complex tooling, unusual testing, or incomplete specifications may require clarification before a firm offer. MOQ begins at one piece, enabling fit checks or engineering samples, but one-piece economics should not be projected onto production demand. NDA support is available for confidential custom parts files. Change control matters after award: material, tolerance, finish, hardware, packaging, or source changes should follow an agreed approval path. PPAP Level 3 can be prepared when requested, but its contents, sample quantity, timing, and customer templates belong in the order scope. Packaging should address part nesting, moisture, edge protection, cosmetic separation, and label traceability rather than being treated as an afterthought. XCWY will not invent customer names, approvals, test reports, or end-product certifications. A disciplined handoff aligns the released design, commercial assumptions, inspection evidence, and shipment method before production begins.
Specifications and Scope
| Quality system | ISO 9001:2015 registration 34025Q30296R0S |
|---|---|
| Operating history | manufacturing support since 1998 |
| Factory scale | capacity within a 15,000 m² facility, six lines, and 78 staff |
| Pressing | press range from 25T through 400T |
| Laser cutting | 12kW limits: carbon steel 25 mm, stainless 20 mm, aluminum 12 mm, copper 6 mm |
| Press brake | forming on a 3,200 mm brake with ±0.5° angle capability under suitable conditions |
| Five-axis machining | precision capability to ±0.005 mm when geometry, setup, and inspection support it |
| Joining | laser, TIG, MIG, and spot welding, plus PEM insertion |
| Inspection | dimensional verification supported by CMM inspection |
Typical Applications
Automotive Mounting Brackets
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
Electrical Contact Supports
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
Appliance Reinforcement Clips
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
Cabinet Hardware
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
Sensor Mounting Tabs
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
Spring Retainers
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
Cable Management Brackets
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
High-Volume Oem Hardware
XCWY reviews this application against the released drawing, material, quantity, interfaces, finish and inspection requirements before proposing a manufacturing route.
What Drives the Cost of a Progressive Stamped Bracket
A stamped bracket carries two cost structures that move in opposite directions. Tooling is a fixed, one-time cost that dominates while volume is low. The piece price is a variable cost that falls as the tool is amortised and press time is spread over more releases. Reading a bracket quotation correctly means separating the two rather than comparing a single number.
Progressive die tooling: published industry ranges
Tooling cost tracks the number of stations, the complexity of the forms and the accuracy required — not part size alone. The ranges below are published third-party industry benchmarks, not XCWY prices.
| Tooling type | Published range | Source |
|---|---|---|
| Simple blanking die | from about $5,000 | Manor Tool (Aug 2026); Jennison (Aug 2025) |
| Brackets under 5 sq in | under $10,000 | Tripar (Jul 2026) |
| Moderate-complexity progressive die | $15,000 – $50,000 | Manor Tool (Aug 2026) |
| Complex multi-station progressive die | $100,000 – $350,000 | Talan Products (Mar 2025) |
| Progressive die, China-based supply | $10,000 – $50,000 | Haizol (Aug 2026) |
| Payment structure | 50% on order, 50% after sample approval | Haizol (Aug 2026) |
Why amortisation matters more than the die price
A published worked example shows the arithmetic that decides a bracket programme. A $25,000 die spread over production falls steadily:
- 10,000 brackets — the tool adds about $2.50 to every piece
- 25,000 brackets — the same tool adds about $1.00 per piece
- 100,000 brackets — the same tool adds about $0.25 per piece
The bracket, the drawing and the die are unchanged across those three rows. Only the volume is different — which is why a tooling quotation and a piece-price quotation for the same bracket are not comparable until both are converted to total programme cost at your realistic annual volume.
Inside the bracket piece price
Published 2026 cost-structure guidance (Haizol) breaks a stamped piece price down roughly as follows.
- Material — 45–55%. Bracket strip width, the nest layout, and the scrap that layout implies.
- Labour — 15–25%. Press speed and how many stations still need a human.
- Overhead — 10–20%. Energy, floor space and tool maintenance.
- Quality — 2–8%. Inspection frequency, first-article and CMM verification.
- Packaging — 2–5%. Bulk packing versus export-grade crating.
Material is the largest line and the most volatile, which is why bracket quotations now carry a shorter validity than they did in calmer markets.
When a progressive die beats fabrication for a bracket
Published side-by-side figures put the crossover between sheet metal fabrication and progressive die stamping at roughly 3,000 to 7,000 parts per year. Below that band, fabrication is usually cheaper on total cost and far more forgiving while a bracket design is still moving. Above it, the die’s advantage grows with every release.
Standards and industry references
- Where a bracket drawing invokes ISO 2768-1, any dimension without an individual tolerance falls back on the nominated general tolerance class — fine, medium, coarse or very coarse. That single decision can turn every untoleranced dimension on the drawing into a potential reject, so it is worth choosing deliberately.
- The Precision Metalforming Association represents a North American metalforming industry worth about $137 billion. It is a useful reference point when weighing whether a bracket programme justifies its own tool, or whether a standard part from the wider supply base does the job.
Questions to settle before releasing a bracket tool
- Who holds title to the die? Confirm ownership, and what happens to any unamortised balance if the programme ends early.
- Who pays for maintenance versus damage? Routine wear and crash damage are different commercial events.
- What is the tool life? Published figures commonly warrant a Western-built progressive die for around a million strikes — check whether your programme sits inside that.
- Is the strip width fixed? A small change in bracket blank size can force a wider coil, which changes both scrap and press selection.
- What is the annual volume band? If honest demand sits under the crossover, a die is the wrong route regardless of the piece price quoted.
- Which tolerances are functional? Tighten only what the bracket’s mounting and interface actually depend on.
About these figures. The tooling ranges, cost shares and volume crossover above are third-party published industry benchmarks, attributed in the tables and text, and are not XCWY prices. Metal prices move; XCWY quotes each bracket against live material prices at the date of quotation, with the material index date and validity window stated on the quote itself.
Risks Buyers Should Resolve Before Release
| Risk | Effect | Control |
|---|---|---|
| progressive pitch error | Define a functional datum and verify the feature at the controlling process stage. | Define a functional datum and verify the feature at the controlling process stage. |
| punch wear | Specify material condition and validate forming with samples before volume release. | Specify material condition and validate forming with samples before volume release. |
| slug pulling | Control weld or forming sequence with appropriate fixtures and an agreed inspection condition. | Control weld or forming sequence with appropriate fixtures and an agreed inspection condition. |
| burr growth | State finish preparation, masking, thickness, and acceptance evidence on the drawing. | State finish preparation, masking, thickness, and acceptance evidence on the drawing. |
| carrier distortion | Use revision-linked hardware identification plus incoming and in-process checks. | Use revision-linked hardware identification plus incoming and in-process checks. |
| springback | Remove or control burrs with direction, edge, and handling requirements. | Remove or control burrs with direction, edge, and handling requirements. |
Manufacturing Evidence
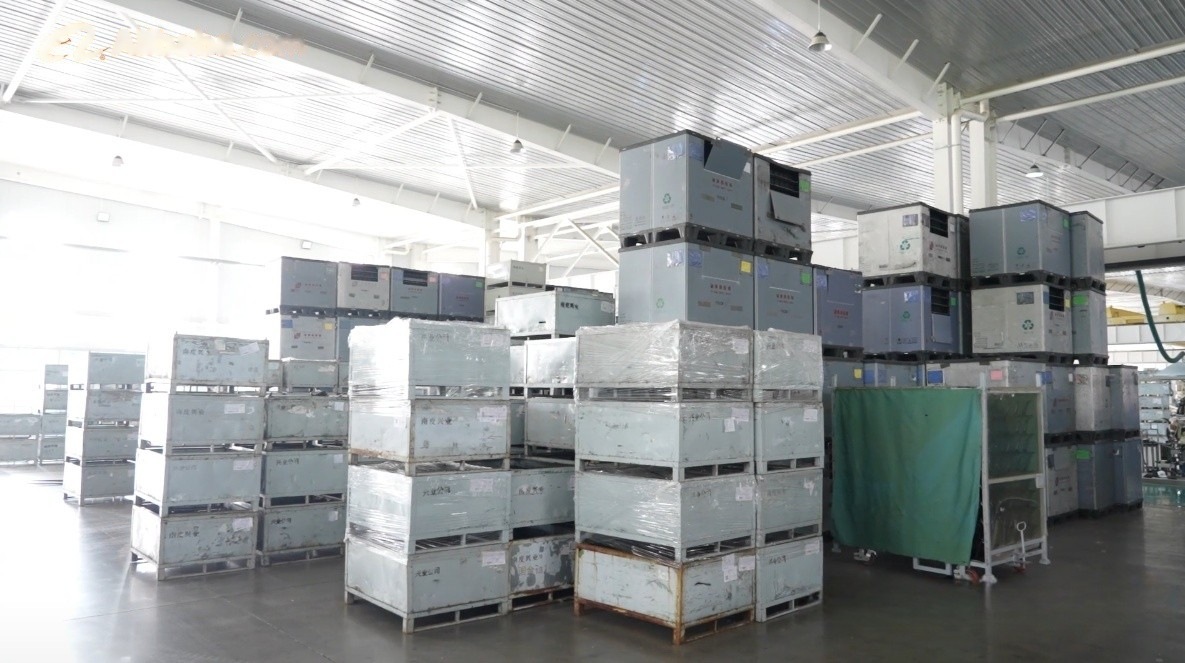
The images below come from the XCWY site asset library and show the plant, equipment, inspection areas and representative parts already published.
Frequently Asked Questions
What files are needed to quote custom parts?
Send the 2D drawing, 3D model when available, quantities, material, finish, tolerance notes, inspection expectations, packaging, and destination. Conflicting revisions should be resolved before a firm quotation.
Can XCWY make a single prototype part?
Yes. The MOQ starts at one piece. Prototype routing may use laser cutting, brake forming, machining, welding, or PEM insertion before dedicated tooling becomes economical.
How quickly can XCWY quote custom parts?
For a complete custom parts RFQ, XCWY targets a quotation within three business hours. Tooling studies, missing standards, unusual tests, or unclear acceptance criteria can extend review.
Which metals are available?
The material range includes CRS, Q235, galvanized steel, SS304, SS316, SS316L, AL5052, AL6061, C110, C260, and 65Mn. Final choice depends on function and released specifications.
Which finishes can be specified?
Available options include powder coating, zinc plating, anodizing, brushing, polishing, and passivation. Compatibility, masking, thickness, appearance, and test requirements should be defined.
Is PPAP available?
PPAP Level 3 is available when requested. Buyers should state templates, submission level, sample quantity, timing, control-plan expectations, and approval workflow in the RFQ.
Which certifications do not apply to custom parts?
XCWY holds ISO 9001:2015 registration 34025Q30296R0S for its quality system. The offer does not claim IATF, ISO 13485, AS9100, or UL certification.
Can XCWY sign an NDA?
Yes. NDA handling is available for confidential drawings, models, tooling data, forecasts, and inspection records before detailed technical review.
Continue the Engineering Review
Get a Manufacturing Review and Quote
Attach the drawing, revision, material, quantity, critical tolerances, finish and target date. The inquiry is saved in the site database and emailed to the XCWY team.